
- Tuo AI

- Live

- My Account
- Shopping Cart
- Inquiry Basket
- Contact Us
- Back to Top




Downspout pipe roll forming machine Solutions & Industrial Equipment
Downspout pipe roll forming machines (downpipe making machines) are specialized automated production lines engineered to fabricate rectangular corrugated downpipes, smooth cylindrical round rainwater pipes, and square drainage leaders. Integrated with continuous longitudinal lockseaming tooling, transverse corrugation presses, and hydraulic cut-off units, these lines process prepainted steel, Galvalume, aluminum, and copper coils with high dimensional precision, delivering turnkey rainwater evacuation solutions for global markets.
 High Precision Downspout Pipe Roll Forming Machine for Gutter Systems
- ztrfm-down spout pipe roll forming machine
$27,000.00
MOQ: 1
 Automatic Downspout Pipe Roll Forming Machine
- ZTRFM-down spout
$19,000.00
MOQ: 1
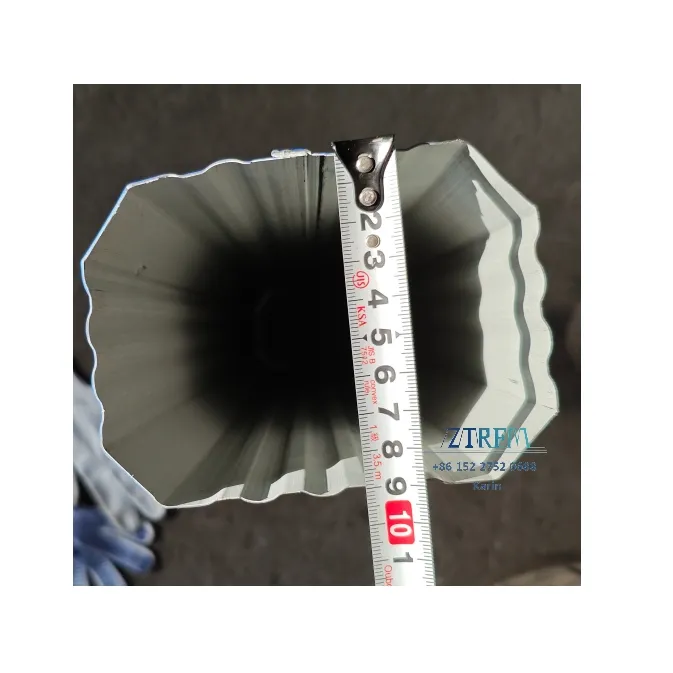 Aluminum Material Roofing Gutter Square Downspout Rain Water Pipe
- 10 m/min+125*90mm+16.5kw
$25,000.00
MOQ: 1
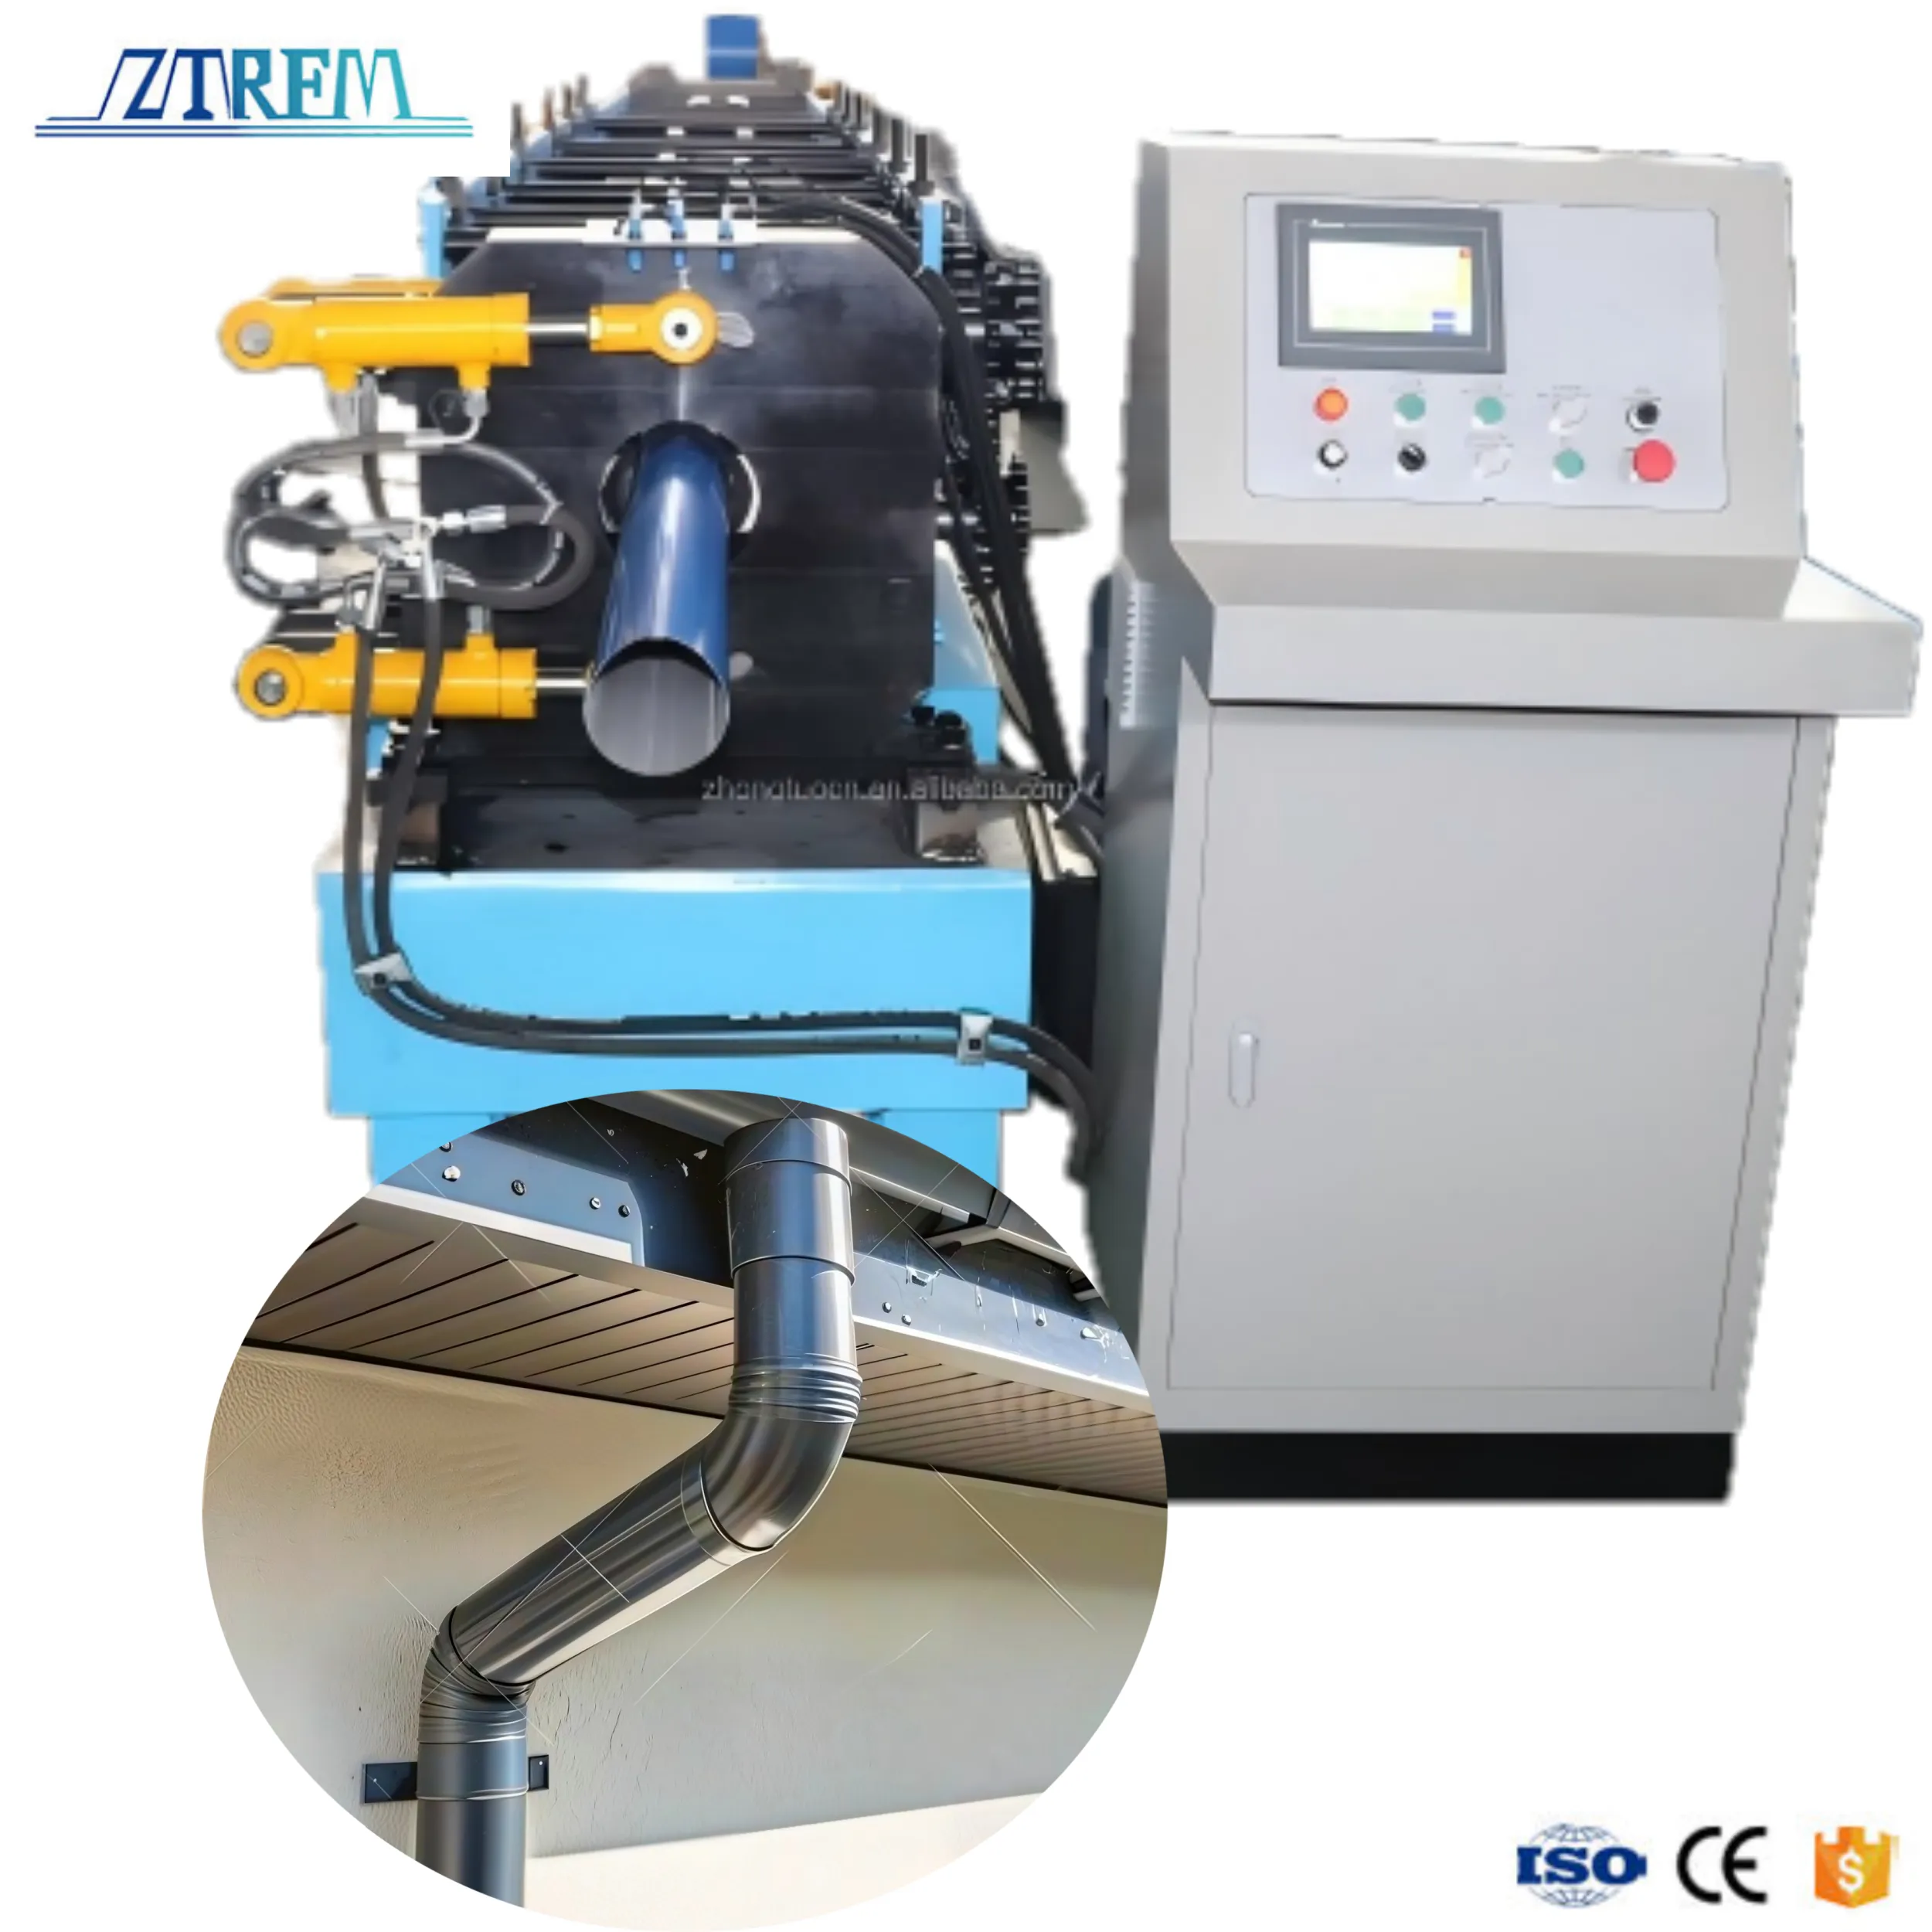 Rain Water Pipe Making Machine Round Rain Pipe Machine Downspout
- Round Rain Pipe Machine Downspout Pipe Machine+7.5KW+15 m/min
$14,000.00
MOQ: 1
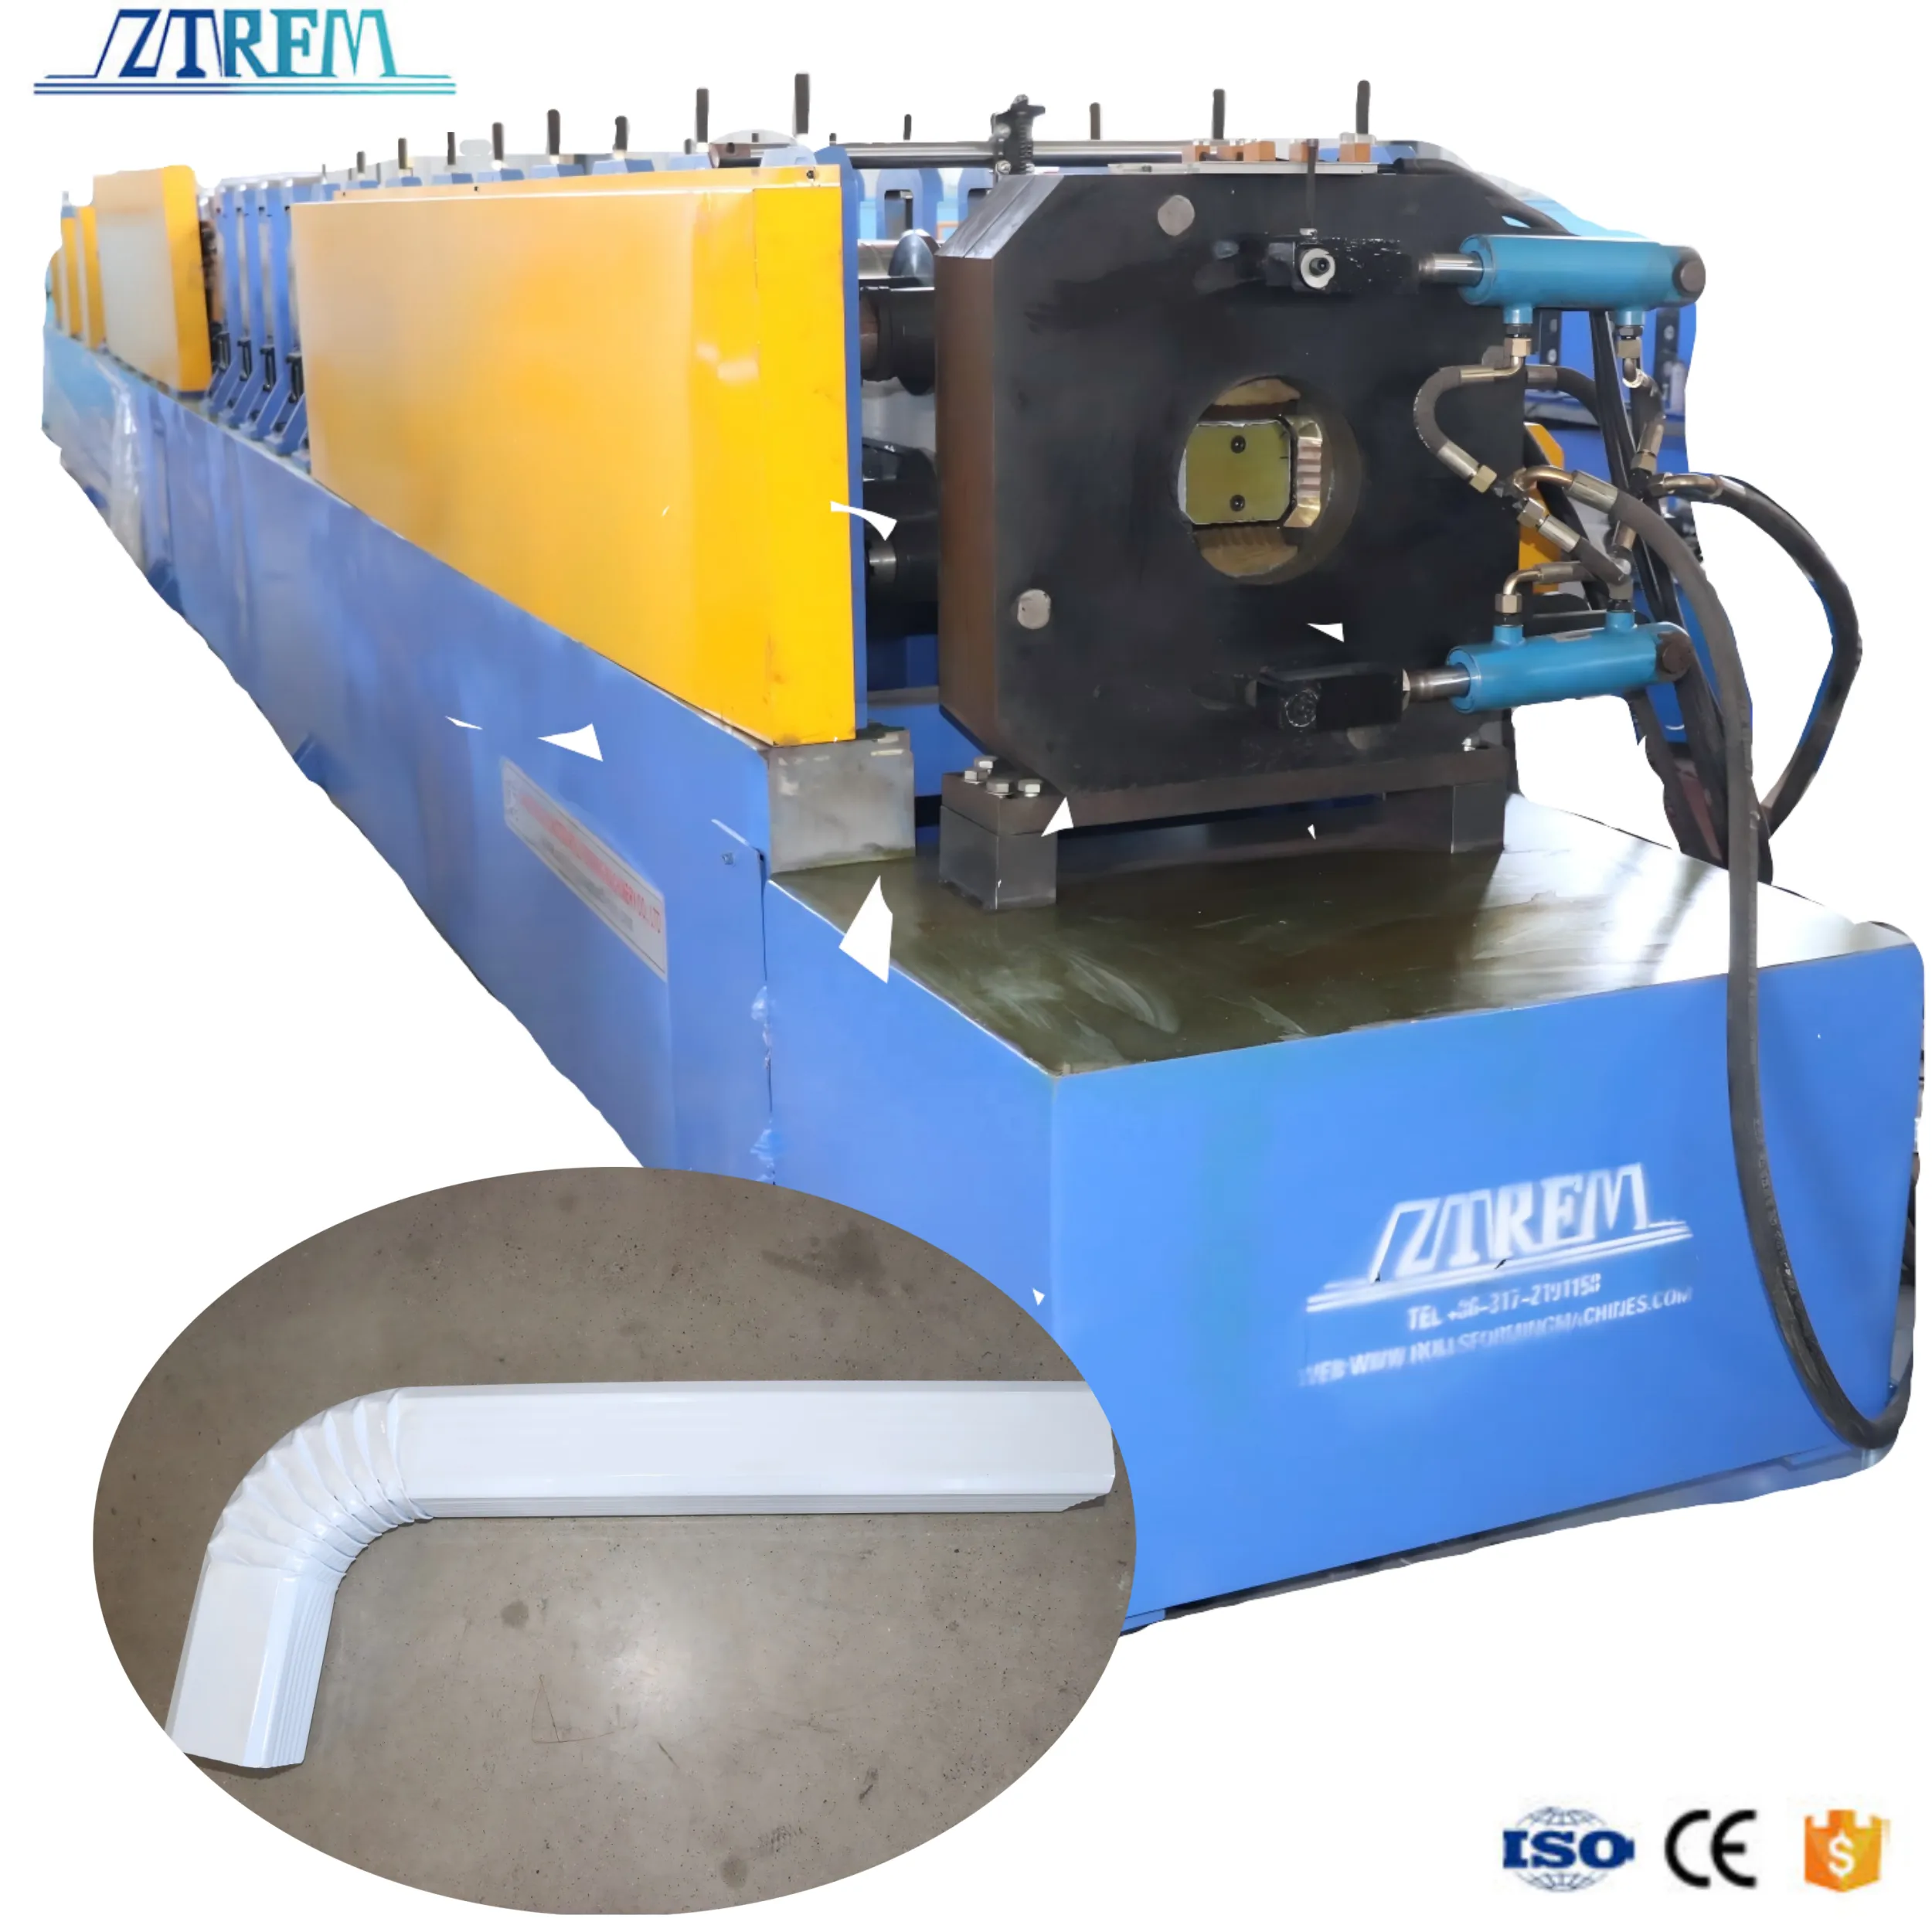 Square Downspout Rain Pipe Machine Downspout Pipe Machine Rain
- 15 m/min+Square Downspout Rain Pipe Machine+7.5KW
$14,000.00
MOQ: 1
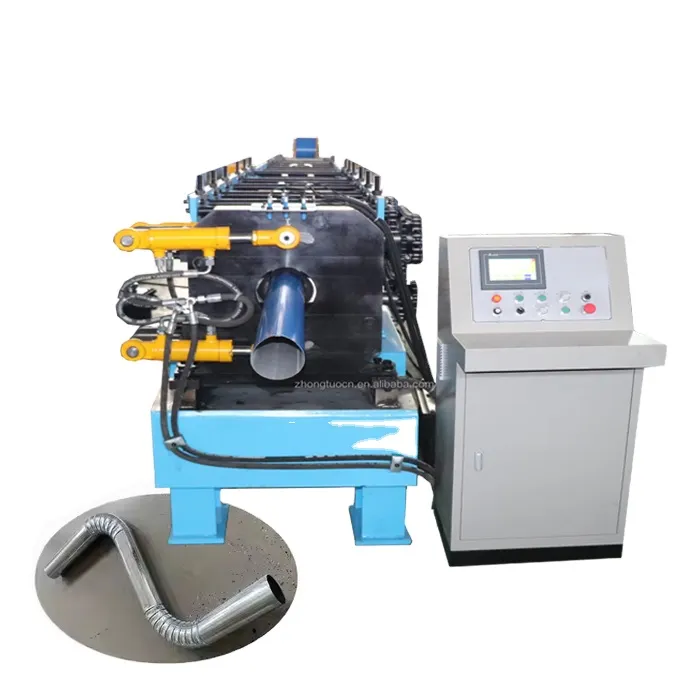 Metal Colored Steel Round Shape Water Downspout Elbow Pipe Tile
- 0-20m/min+RD+7.5kw
$20,000.00
MOQ: 1
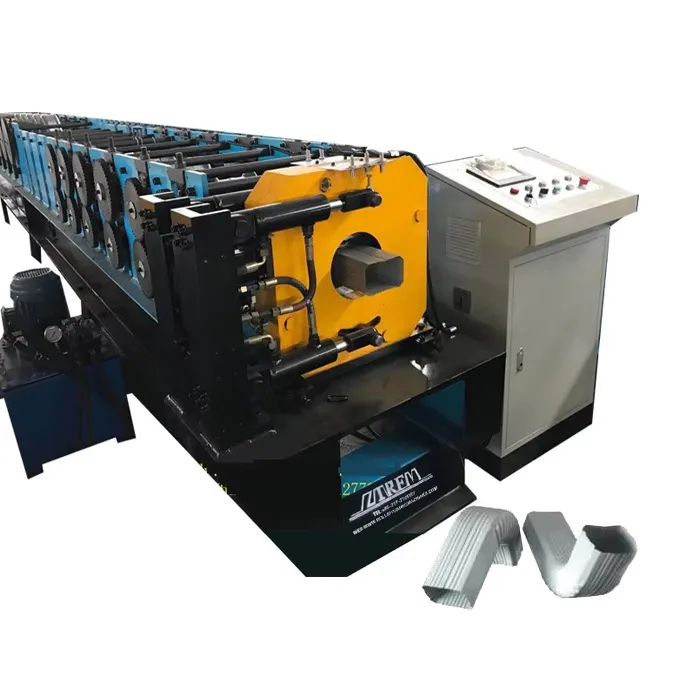 Metal Rain Gutter Downspout Elbow Roll Former Machine
- 0-20m/min+5.5kw
$20,000.00
MOQ: 1
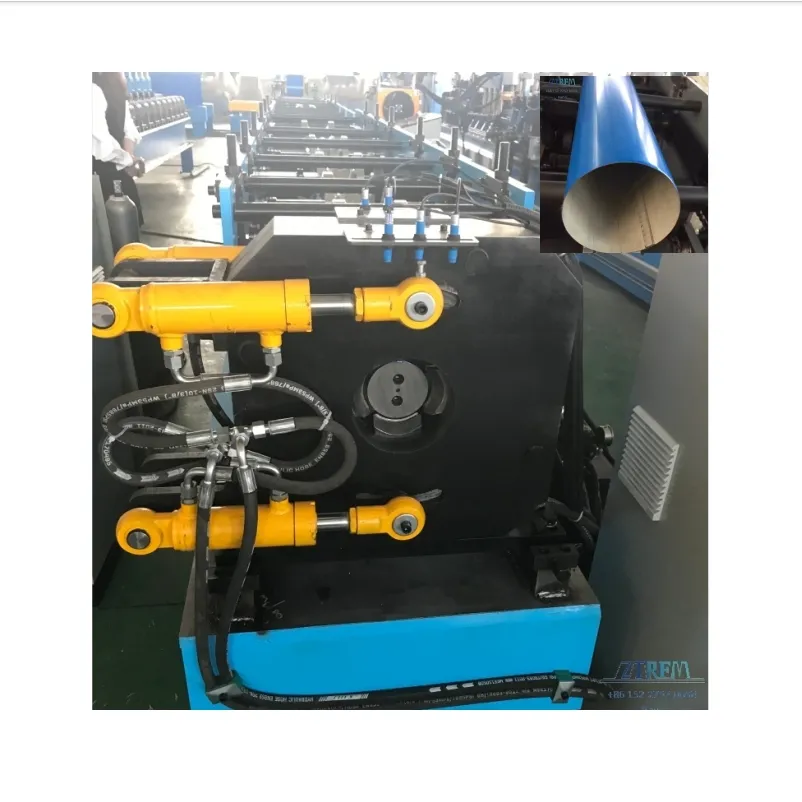 Roofing Gutter Round Rain Downspout Water Pipe Aluminum Roll
- DS50+16.5kw
$28,000.00
MOQ: 1
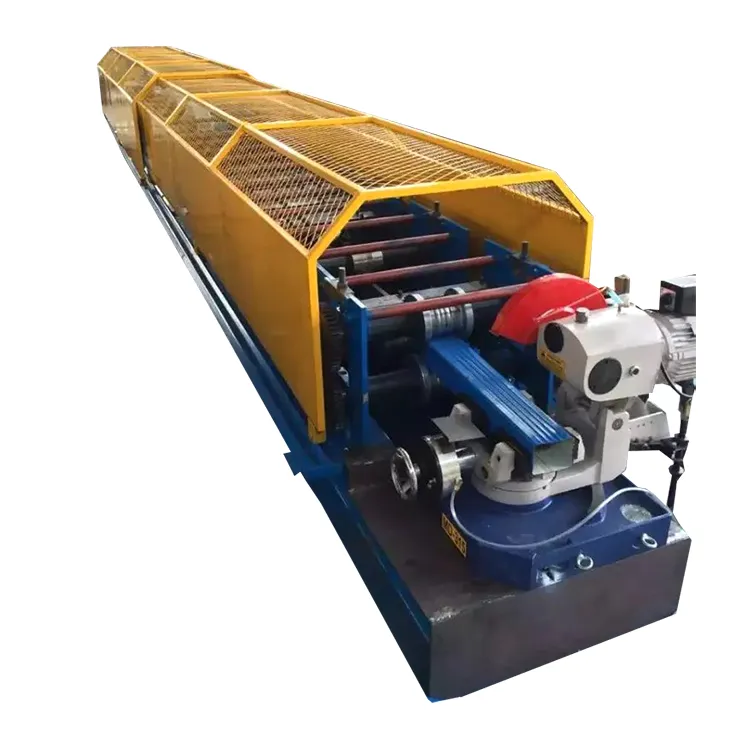 Downspout Gutter Elbow Making Roll Forming Machine
- DS50+16.5kw
$26,000.00
MOQ: 1
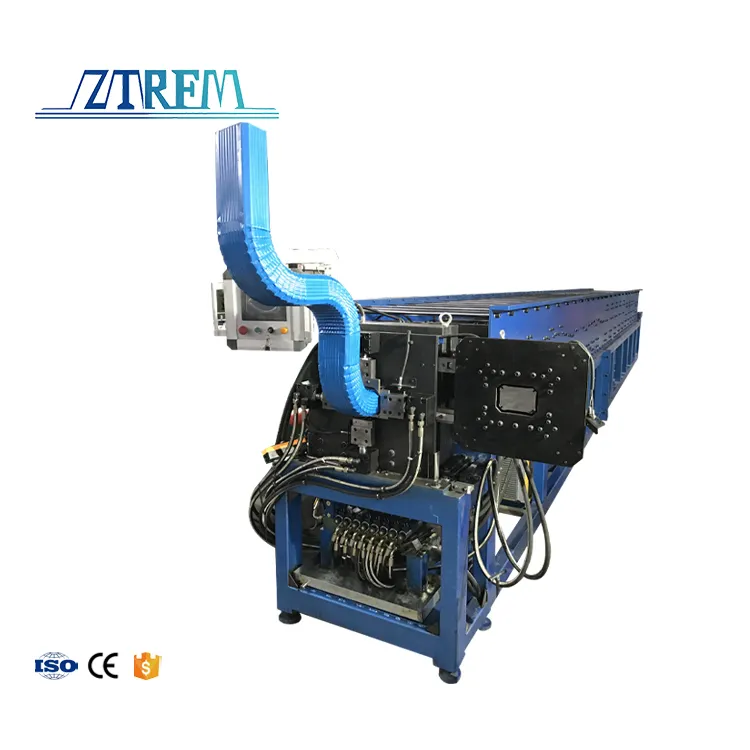 Gutter Coil Aluminum Making Machine Roofing Gutter Making Machine
- 10 m/min+DS50+16.5kw
$28,000.00
MOQ: 1
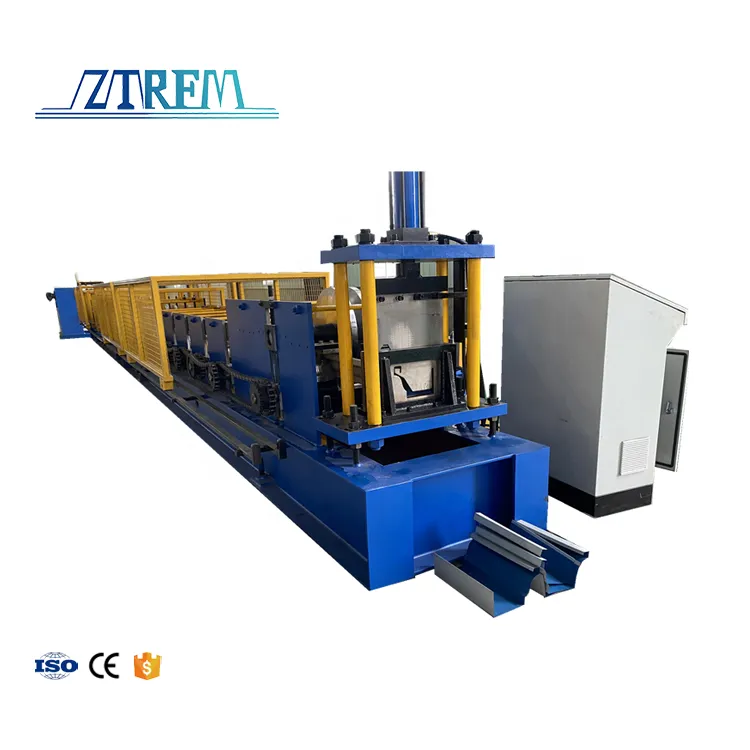 Gutter Coil Aluminum Making Machine Roofing Gutter Making Machine
- 8KW+15 m/min
$11,000.00
MOQ: 1
 Rain Gutter Downspout Roll Forming Machine Downspout Machine square
- Rectangular Downspout Making Machine
$22,999.00
MOQ: 1
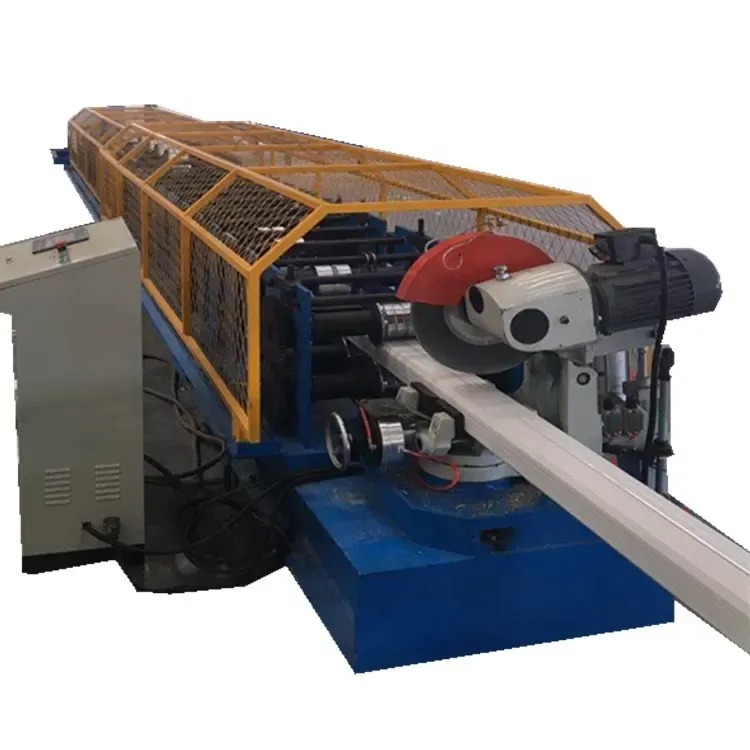
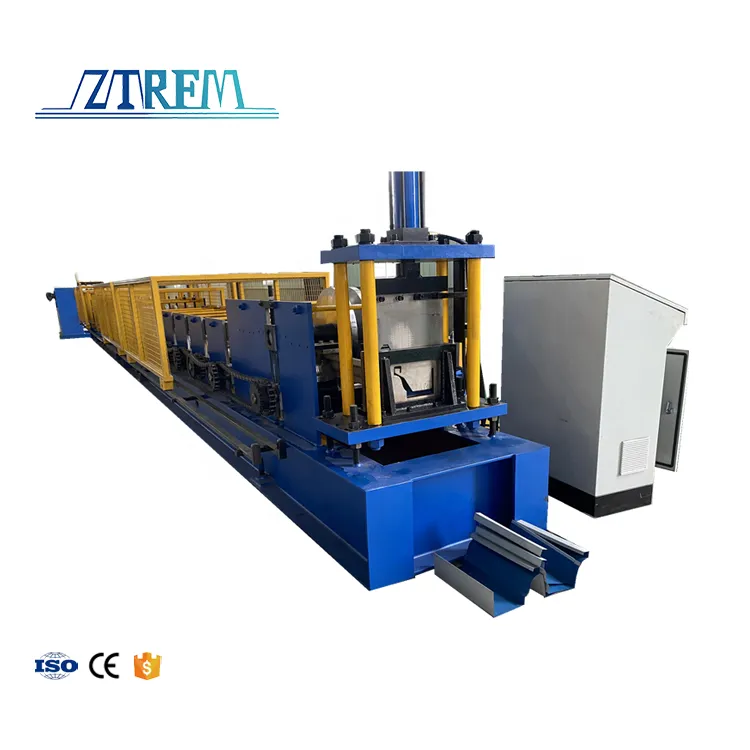
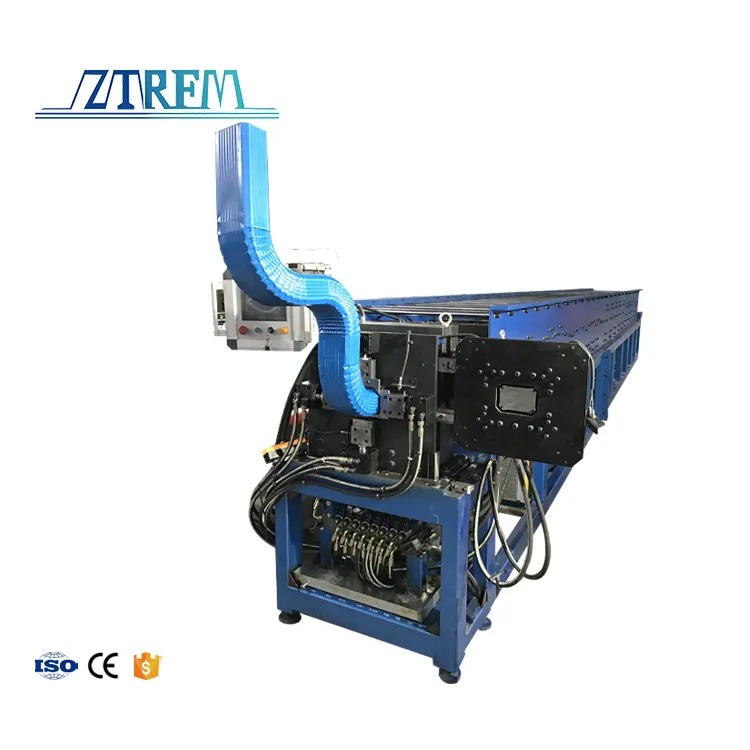
 ZhongTuo Automatic Square Downspout Rainwater Pipe Roll Forming Machine ZTRFM Automatic Metal Downpipe Forming Machine
- ZTRFM Automatic Metal Downpipe Forming Machine
$25,000.00
MOQ: 1




About Downspout pipe roll forming machine Solutions & Industrial Equipment
Downspout pipe roll forming machinery represents an indispensable partner to gutter manufacturing, transforming continuous flat metal strip into rigid, hollow rainwater vertical leader pipes. In modern rainwater systems, downspouts must withstand internal water hydrostatic pressure, freezing ice expansion, and external wind vibrations while maintaining an aesthetically pleasing exterior finish that complements building wall claddings and corner columns.
The roll forming process utilizes 18 to 26 progressive cold-forming passes. Starting from precision-slit metal coil strip, the initial stands shape the profile flanges and prep the lockseam edges. Intermediate stations gradually fold the sheet into a closed rectangular or round tube, while specialized rotary closing wheels press and interlock the continuous longitudinal mechanical lockseam (Pittsburgh or standing seam). For rectangular models, an inline hydraulic or eccentric press station stamps decorative and structural transverse corrugations that enhance pipe wall rigidity and accommodate freeze-thaw thermal expansion.
Advanced equipment lines feature automated end-shrinking (swaging) mechanisms that slightly reduce one end of each cut pipe, enabling quick socket-and-spigot push-fit field assembly without separate couplers. Complementary standalone or inline hydraulic elbow machines crimp downpipes into smooth 75-degree or 90-degree offset elbows. Controlled via Siemens PLCs and optical digital encoders, these high-speed lines achieve production speeds of 10–15 m/min with tight length tolerances of ±1.0 mm.
Applications
Rectangular Corrugated Seam-Locked Downpipe Production
Continuous cold roll forming lines manufacturing rectangular downspouts with longitudinal lockseams and transverse corrugations for residential construction. Applications: Residential suburban homes, architectural multi-family housing, and commercial building perimeter drainage. Features: Continuous internal lockseaming roll passes, automated corrugated rib press station, and hydraulic distortion-free cut-off.
Round Spiral Lock-Seam Architectural Rainwater Pipe Lines
High-speed roll forming machines that produce round cylindrical downpipes with tight external standing seams or flush internal lockseams. Applications: Contemporary commercial office buildings, civic cultural centers, and luxury residential estates. Features: Smooth cylindrical round forming stations, high-integrity airtight seam locking, and compatible round elbow pipe joints.
Integrated Hydraulic Elbow Bending & Downspout Shrinking Cells
Downstream automated finishing units paired with downpipe roll formers, performing hydraulic 75°/90° elbow crimping and pipe end swaging/flaring. Applications: Turnkey rainwater system manufacturing plants, prefabricated drainage accessory shops, and export factories. Features: Automated pipe end shrinking for seamless push-fit interlocking, multi-angle hydraulic elbow crimping, and rapid cycle times.
Industrial High-Bay Logistics Siphonic Rainwater Downpipe Systems
Heavy-duty roll forming machines producing heavy-gauge large-diameter downpipes engineered for siphonic full-bore roof drainage systems. Applications: Wide-span airport passenger terminals, mega logistics warehouses, and sports stadium roofs. Features: High negative pressure vacuum rating, high-yield steel strip roll forming, and robust welded or high-compression locked seams.
Architectural Pure Zinc & Copper Heritage Downpipe Forming Lines
Precision non-marking downspout roll forming lines engineered specifically to form natural architectural copper and titanium-zinc rainpipes without tool marks. Applications: Historic cathedral restorations, luxury palace estates, and elite museum architecture. Features: Zero-friction urethane-sleeved forming passes, precise seam alignment, and compatibility with classical decorative rainwater hopper heads.
Technical Overview
| Parameter | Information |
|---|---|
| Machine Architecture | Continuous Tube Roll Forming Line with Longitudinal Lockseamer & Swaging Unit |
| Downpipe Shapes & Sizes | Rectangular (2"x3", 3"x4", 4"x5"), Round (Ø 75–125 mm), Square (75x75, 100x100 mm) |
| Material Thickness Capacity | Steel / Galvalume: 0.40 – 0.70 mm; Aluminum: 0.50 – 0.90 mm; Copper: 16–20 oz |
| Coil Strip Width Range | 200 mm – 450 mm (Profile dependent) |
| Forming Stations Count | 18 – 26 progressive stations including lockseam closing and sizing passes |
| Production Line Speed | 10 – 15 m/min (Continuous running with automated hydraulic cut-off) |
| Roller Material & Heat Treatment | Forged 45# / Cr12MoV, Hard Chrome Plated (0.05 mm), Mirror Polished HRC 58–62 |
| Lockseam Type | Continuous mechanical fold lockseam (Internal or External standing lock) |
| Cut-Off & Swaging System | Hydraulic non-deforming clamp shear with automatic end shrinker unit |
| Automation Control System | PLC + Touchscreen HMI + Digital Rotary Encoder, length precision ±1.0 mm |
Related Solutions
Gutter and Downspout Roll Forming Solution
Paired rainwater package: K-style / half-round gutter plus lock-seam downpipe, w…
Rainwater System Solution: Gutters, Elbows & Covers
A rainwater shop is a gutter mill plus fittings. Volume K-style or half-round ru…
Tube & Pipe Processing Solution
Pipe-making is several hosts: ERW round/square, lockform duct, a recipe tube (ZP…
Metal Roofing & Wall Panel Roll Forming Solution
Trapezoidal / IBR, standing-seam, corrugated or glazed-tile roof and wall panel…
Custom Profile Roll Forming for OEM
Flexible roll forming line for custom cross-sections. Suitable for OEMs who need…
Metal Sheet Processing Solution
Blanking and cut-off around a roll former is a shear class: flying (tracking) sh…
Related Information

Downpipe and Gutter Roll Forming Machine: Profiles, Sizes and Production Line
Downpipe sizes (2x3, 3x4, 4x5), K-style vs rectangular gutters, machine configur…
Read More
Gutter & Downpipe Roll Forming Machine: K-Style, Box and Half-Round Lines
gutter roll forming machine, downpipe roll forming machine, k style gutter machi…
Read More
Innovations in Cold Roll Forming Machinery: Smart Manufacturing Solutions
By Hu Xianzhe, Cold Roll Forming Technical Engineer at ZTRFM | Last Updated: Sep…
Read More
What Is a Roll Forming Machine? Core Principles and Industrial Applications
By Iris Xu, Sales Engineer at ZTRFM | Last Updated: September 15, 2026 Roll form…
Read More
How to Choose a Roll Forming Machine: 7 Key Factors for B2B Buyers (2026)
A practical B2B checklist for selecting a roll forming machine: profile, materia…
Read More
Roll Forming Machine Price Guide: Cost Factors, Ranges and How to Get Accurate Quotes (2026)
Cost factors that affect roll forming machine pricing and how B2B buyers can req…
Read More
FAQ
What downspout pipe shapes and dimensions can be produced?
Machines produce standard rectangular downpipes (2"x3", 3"x4", 4"x5"), round downpipes (Ø 75 mm, Ø 90 mm, Ø 100 mm, Ø 125 mm), and square architectural downpipes with either smooth or corrugated walls.
How is the longitudinal lockseam formed and sealed?
The longitudinal seam is formed progressively through closing rollers that fold and squeeze the male and female edges into a continuous, watertight mechanical lockseam without welding.
Can the machine produce downpipes with corrugated accordion walls?
Yes, lines include an integrated transverse corrugating press station that presses decorative and strengthening ribs into the pipe walls before or after seam closure.
How do pipe ends fit into one another during field installation?
An automated hydraulic swaging (shrinking) station compresses 50 mm of one end, reducing its perimeter slightly so it inserts snugly into the unswaged end of the next pipe segment.
What elbow bending equipment is paired with downspout roll forming lines?
We provide companion hydraulic downspout elbow machines that grip the pipe and perform synchronized mechanical crimps to form precise 45°, 75°, or 90° bends with matching aesthetics.
What materials can be run on downpipe roll forming machines?
The machines run PPGI prepainted steel, Galvalume (0.4–0.7 mm), aluminum alloys (0.5–0.9 mm), pure copper (16 oz / 20 oz), and titanium-zinc sheet coils with non-marking tooling.
What cutting system is standard to prevent collapsing the hollow tube?
The line uses a hydraulic circular or rectangular internal-external clamping shear with dual opposed blades that sever the thin-walled tube cleanly without flattening the hollow cross-section.