
- Tuo AI

- Live

- My Account
- Shopping Cart
- Inquiry Basket
- Contact Us
- Back to Top




Solar Panel Bracket Roll Forming Machines
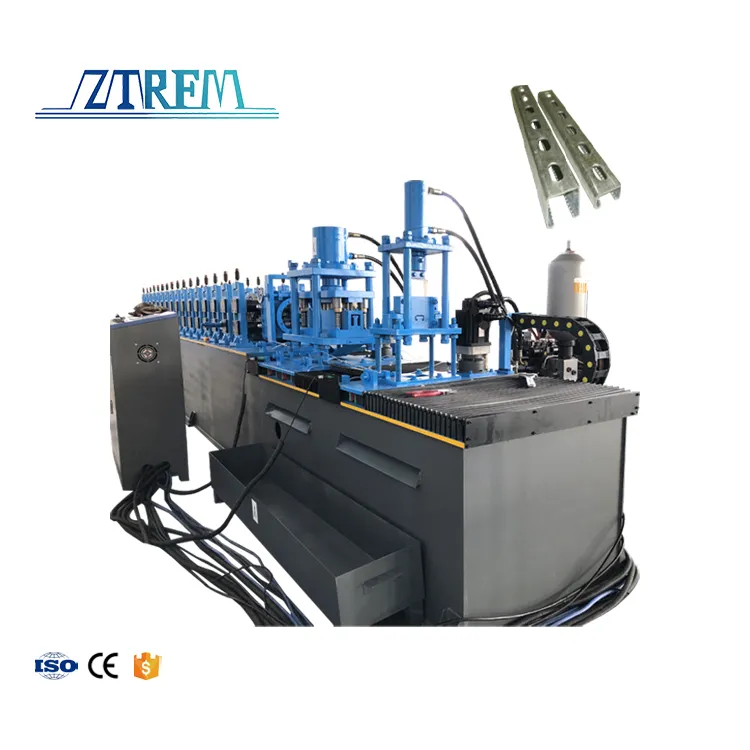
Solar panel bracket roll forming machines continuously produce cold-formed mounting rails, strut channels (Unistrut type 41×41 / 41×21 mm), solar tracker torque tubes, and ground-mount C/U posts for the global renewable energy industry. Engineered to process high-strength galvanized steel and Zinc-Aluminum-Magnesium alloy (ZAM) coils (1.5 mm to 3.0 mm thick), these automated lines feature high-speed servo hydraulic pre-punching presses executing continuous slotted, round, and serrated teeth patterns. Equipped with 16 to 22 precision roll forming stations and synchronized flying shears, solar bracket machines ensure tight hole pitch tolerances and high throughput. Explore technical specifications, tooling capabilities, and turnkey production line solutions below.
Filters
- Certification
 Anti-vibration Rolling Forming Machine PV Support Bracket Multi
- 20m/min+ZTSS+2000
$30,000.00
MOQ: 1
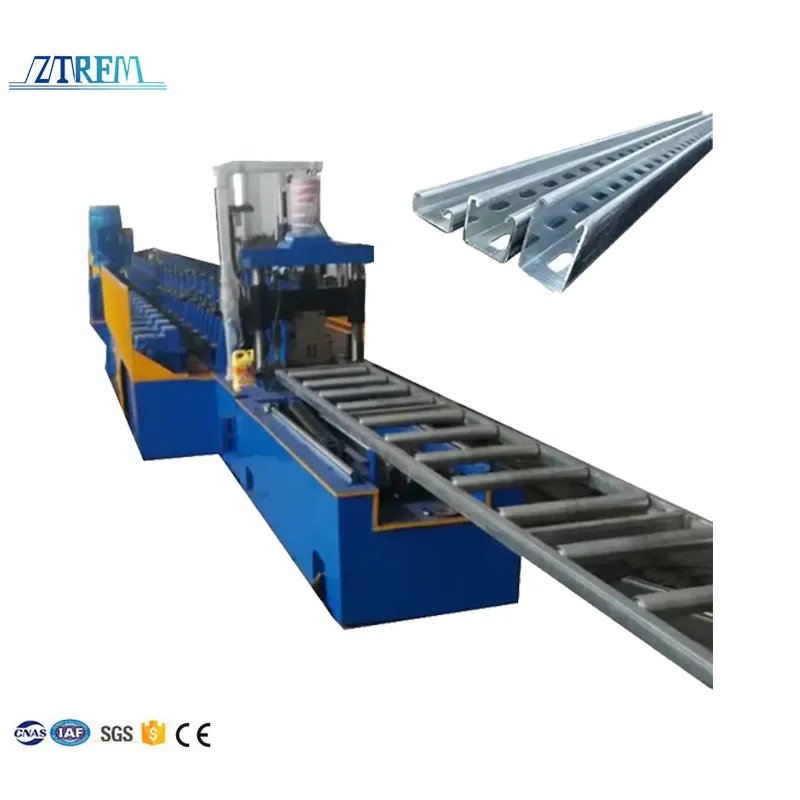 Adjustable Different Sizes Solar Panel Mounting Bracket Profile
- 4500+PLC, Motor, Gear, Bearing, Pump, Engine+Hebei,China+2 Years+ZTRFM
$28,000.00
MOQ: 1
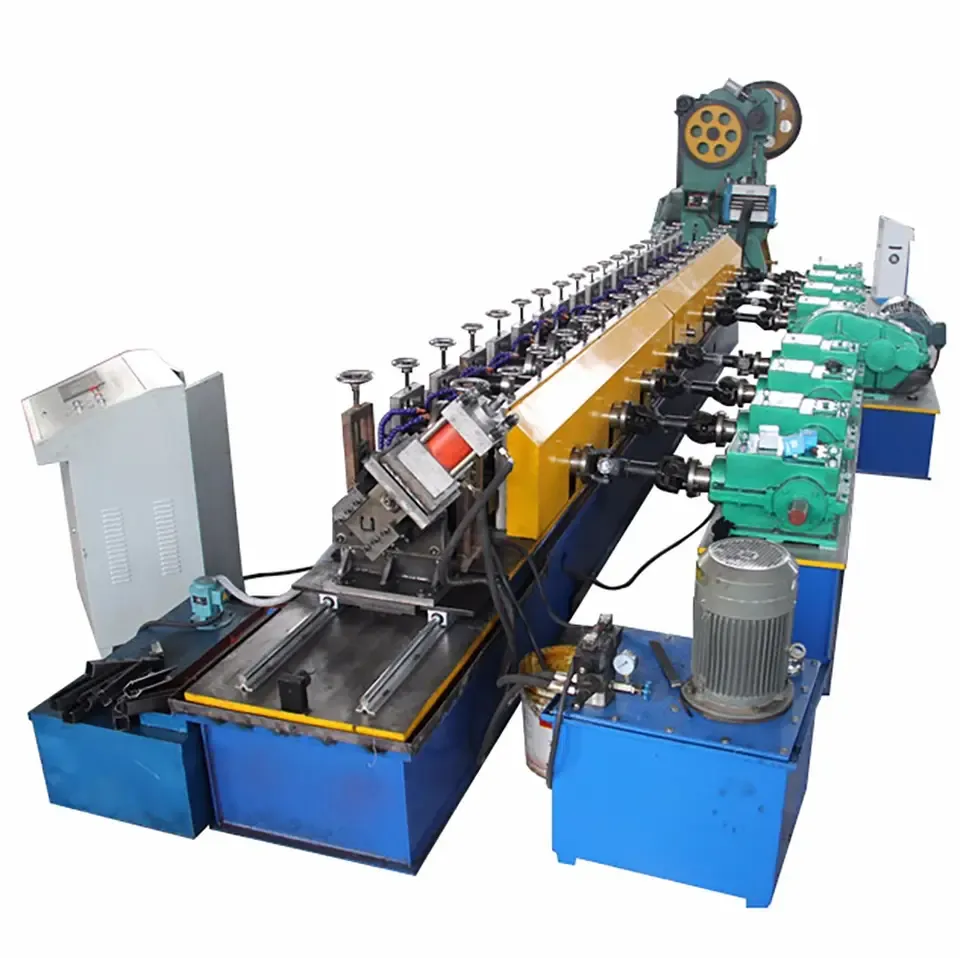 Stent U Bracket Solar Panel Mounting Structure Roll Forming Machine
- 4500+PLC, Motor, Gear, Bearing, Pump, Engine, Engine+Hebei,China+1 Year+ZTRFM
$65,000.00
MOQ: 1
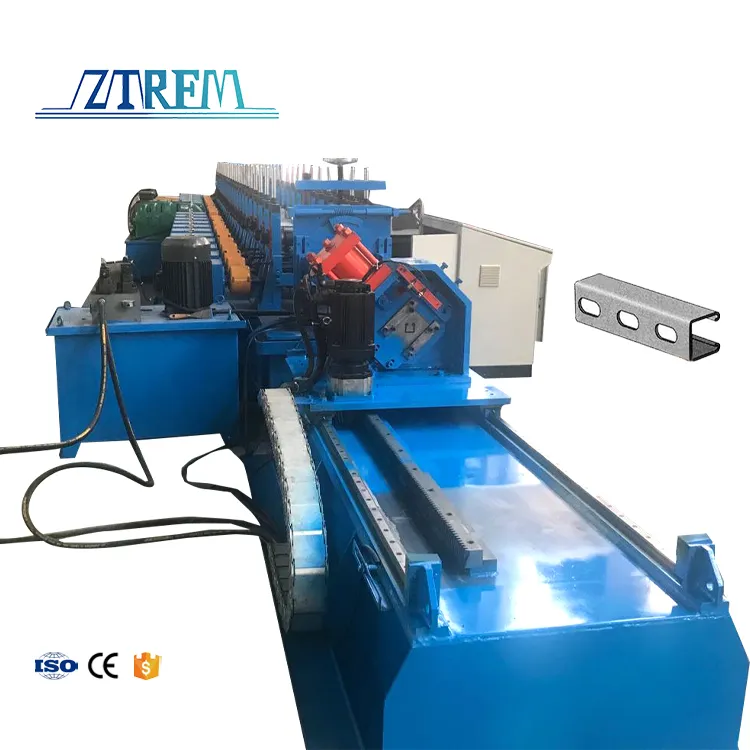 Solar Panel Mounting Structure Roll Forming Machine Solar Panel
- 10-15m/min+solar panel farme roll forming machine+15kw
$35,000.00
MOQ: 1
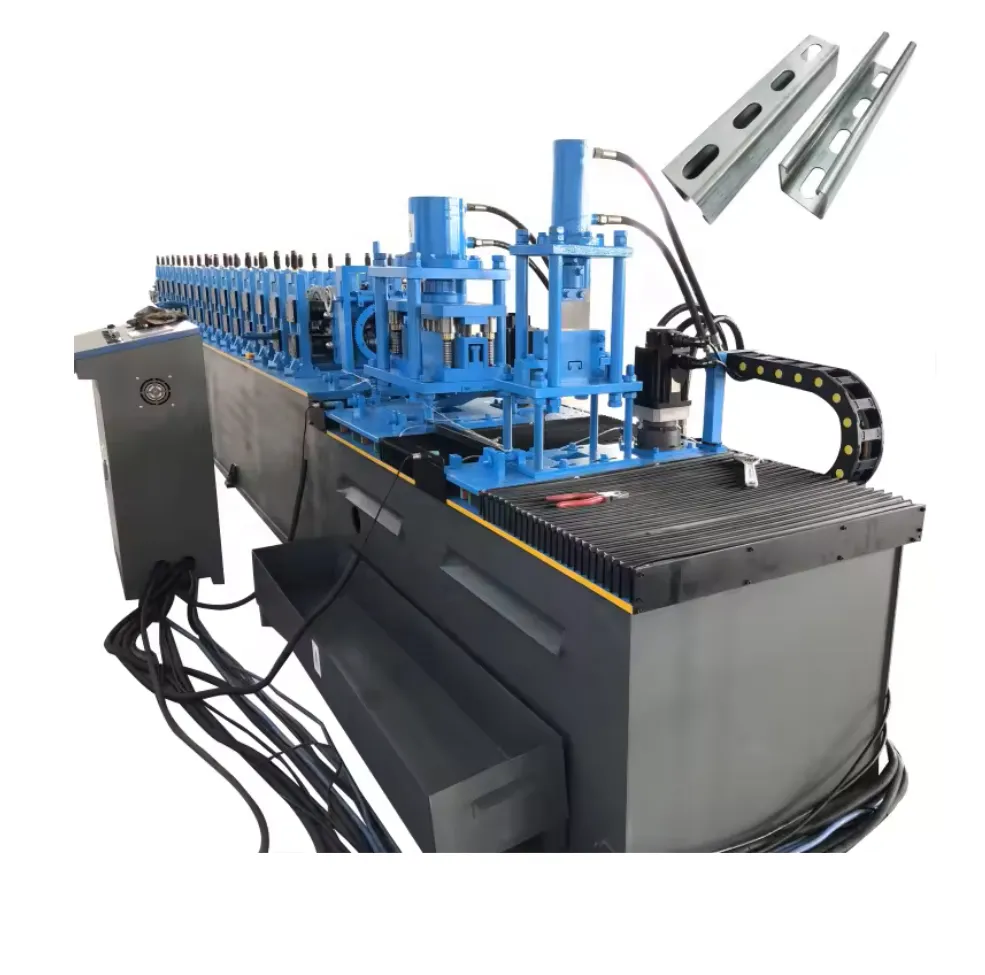 Solar Rack / Solar Panel Mounting Roll Forming Machine 41x41
- 15 m/min+22kw
$31,000.00
MOQ: 1
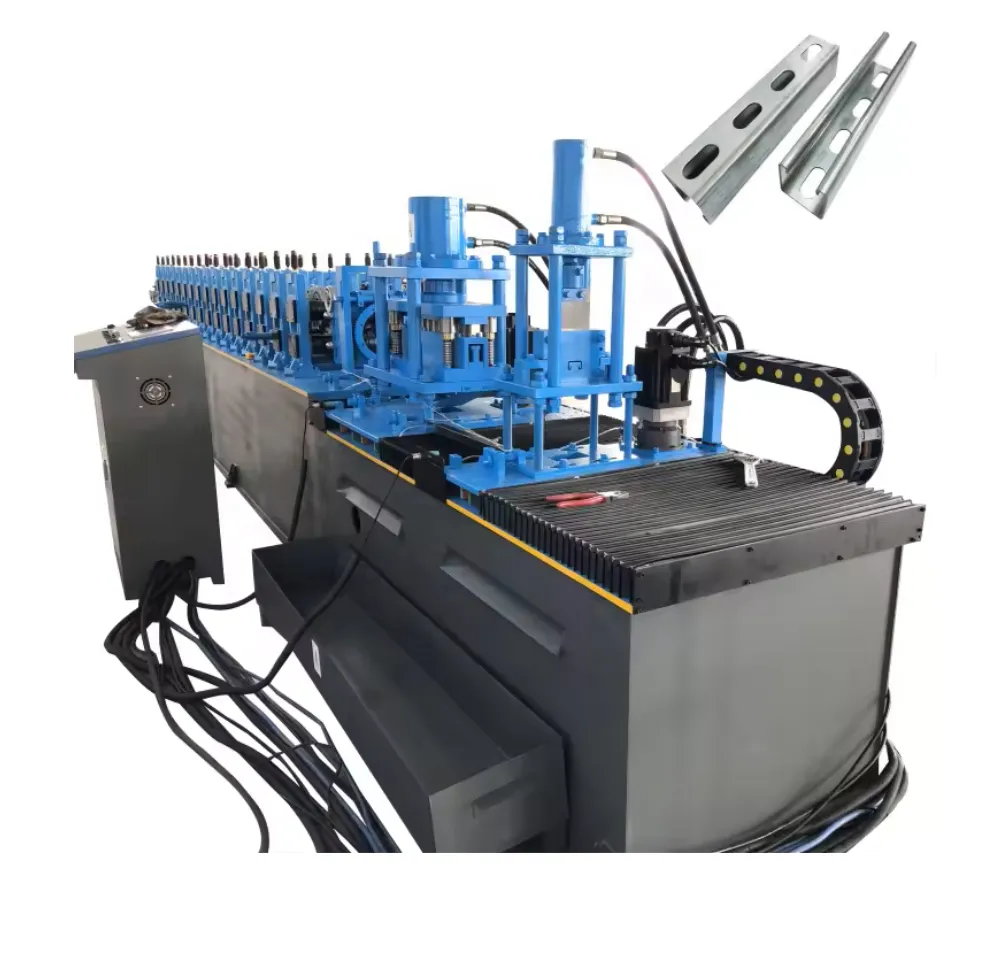 Metal Slotted C U Profile Unistrut Solar Strut Channel Roll
- 15 m/min+ZTRFM-S11+22kw
$31,000.00
MOQ: 1
 Solar Strut Frame Support Pillar Roll Forming Machine & Cutting
- 20m/min+ZTSS+1500MM
$30,000.00
MOQ: 1
 Solar Strut Channel Roll Forming Machine Solar Mounting Structure
- Solar Strut Channel Machine
$16,600.00
MOQ: 1
 Precision Solar Roof Tiles Shingles Solar Panel Bracket Roll
- 25 m/min+ZTRFM Solar Panel Bracket Roll Forming Machine+940
$11,000.00
MOQ: 1
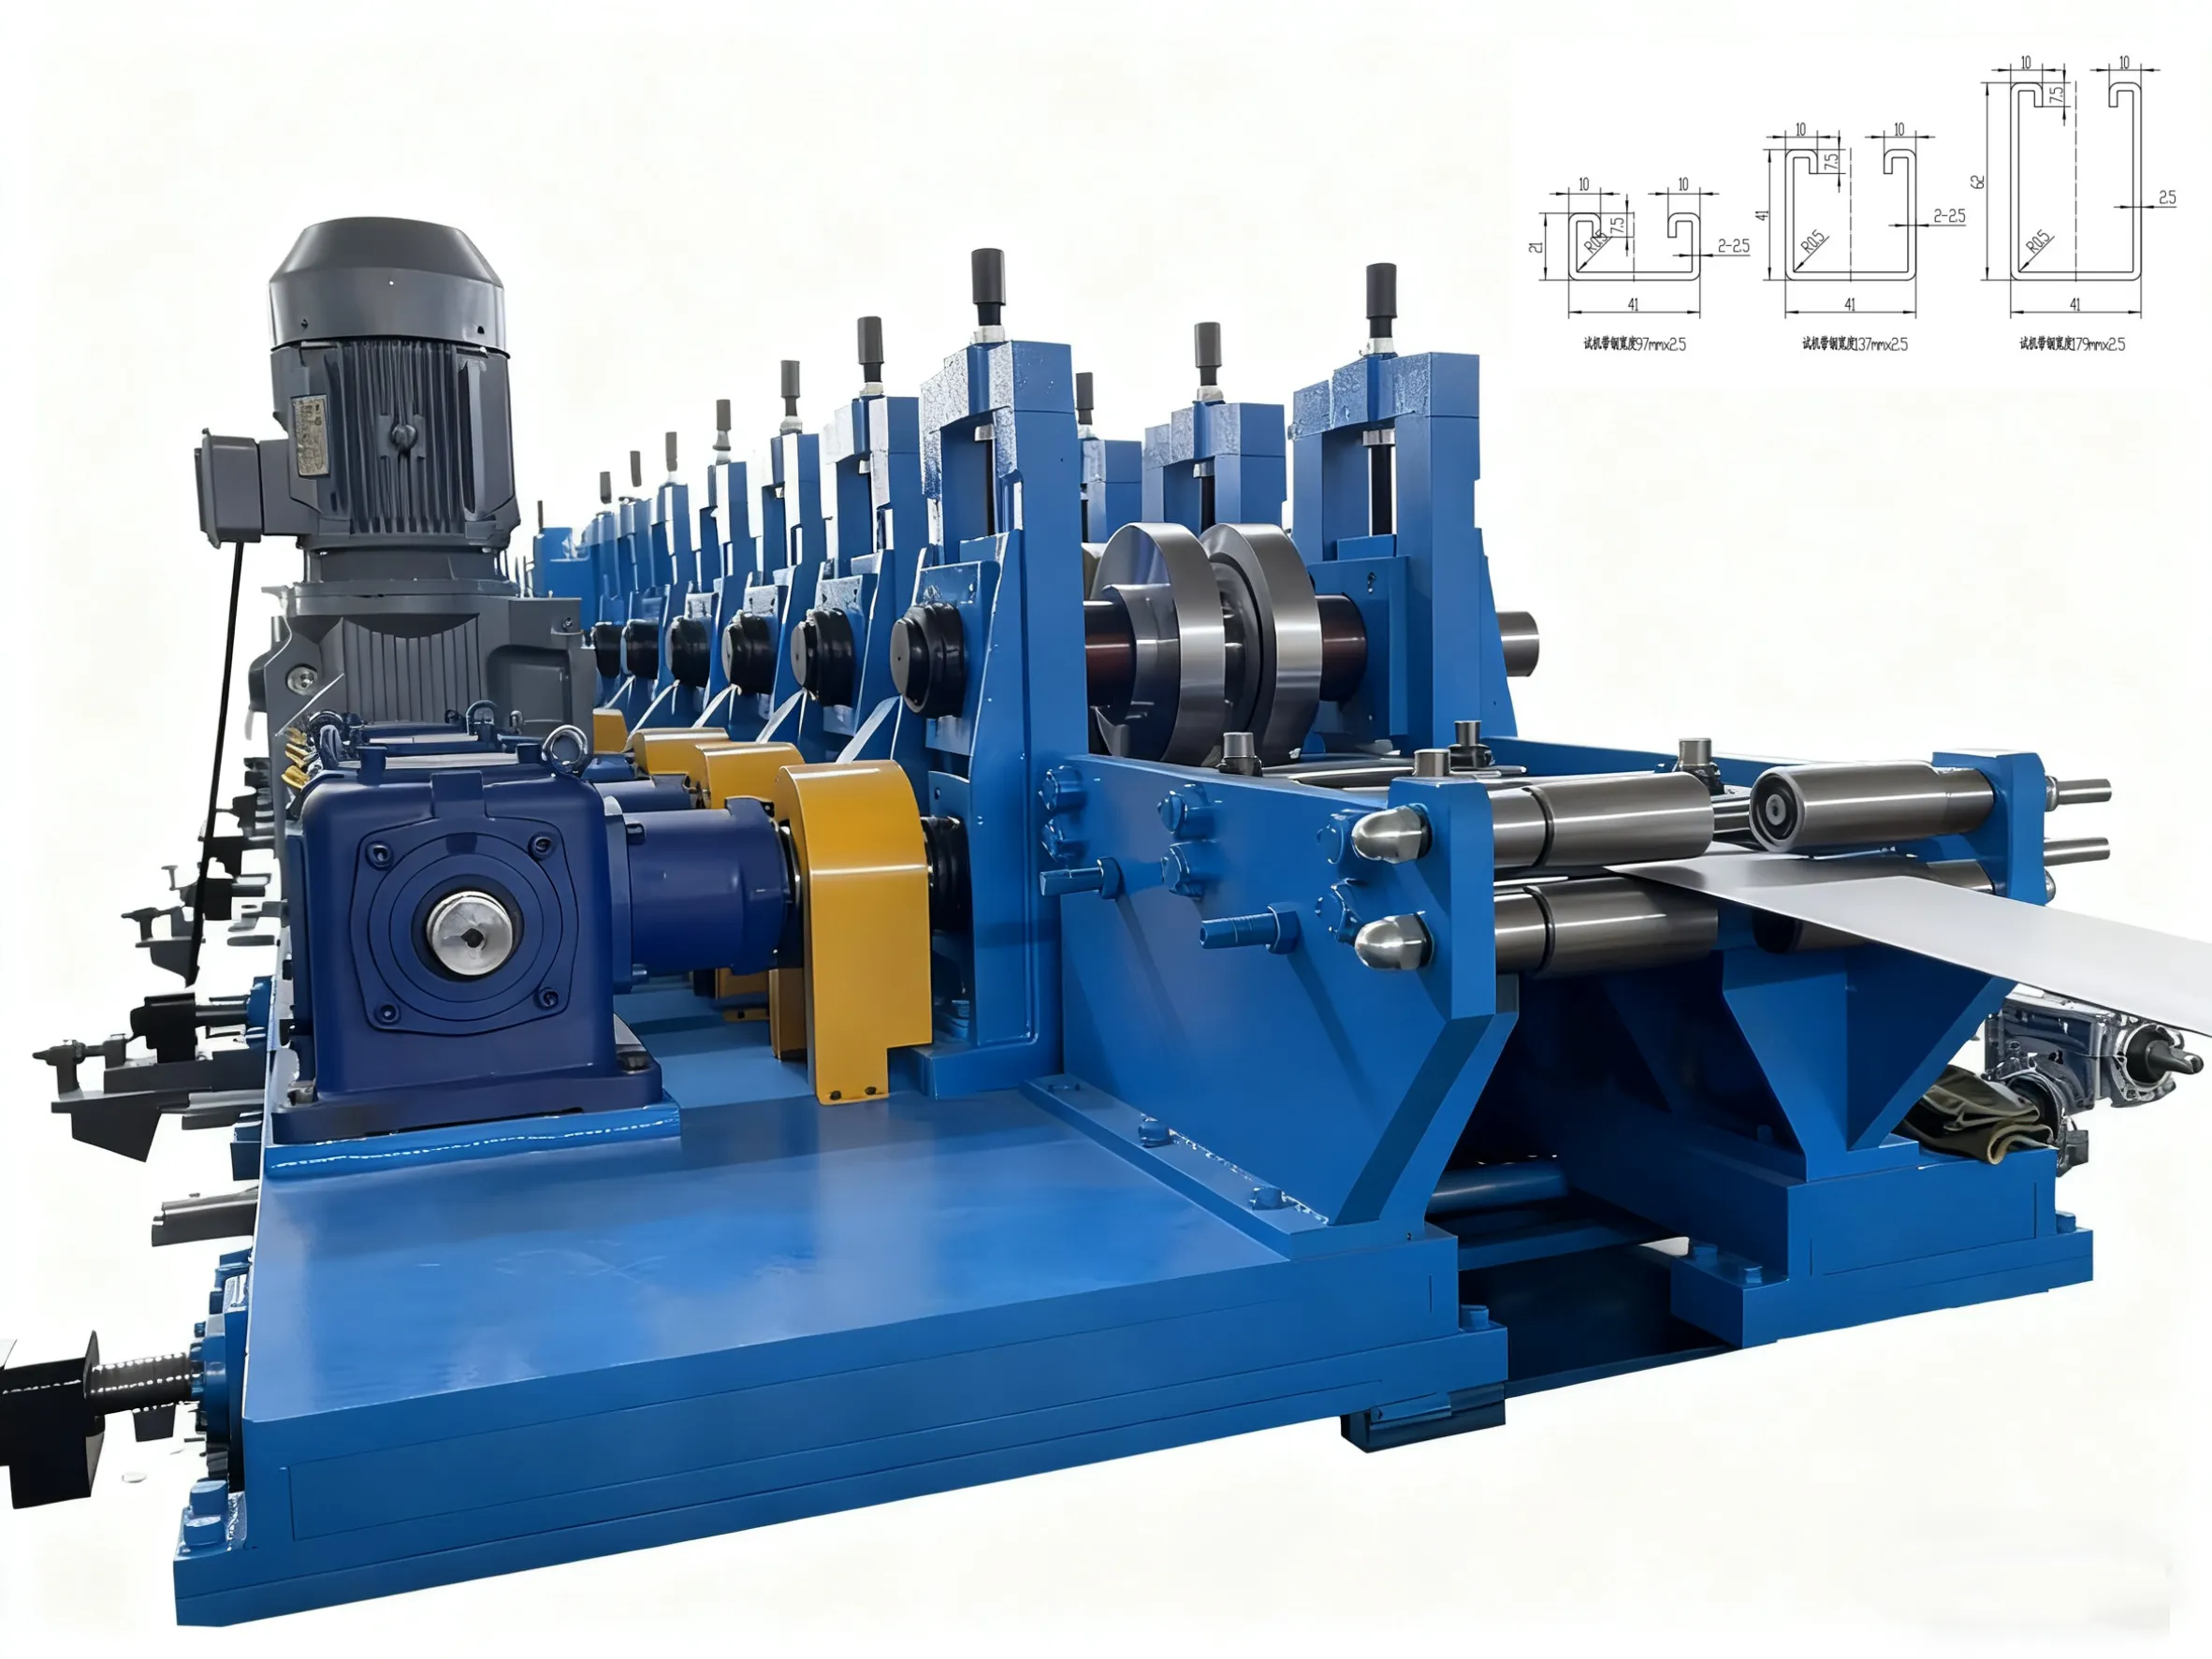 Multiple Size 41x21 41x41 41x72 Solar Panel Mounting Machine
- 20 M/Min+ZT21-72+78kw
$102,000.00
MOQ: 1
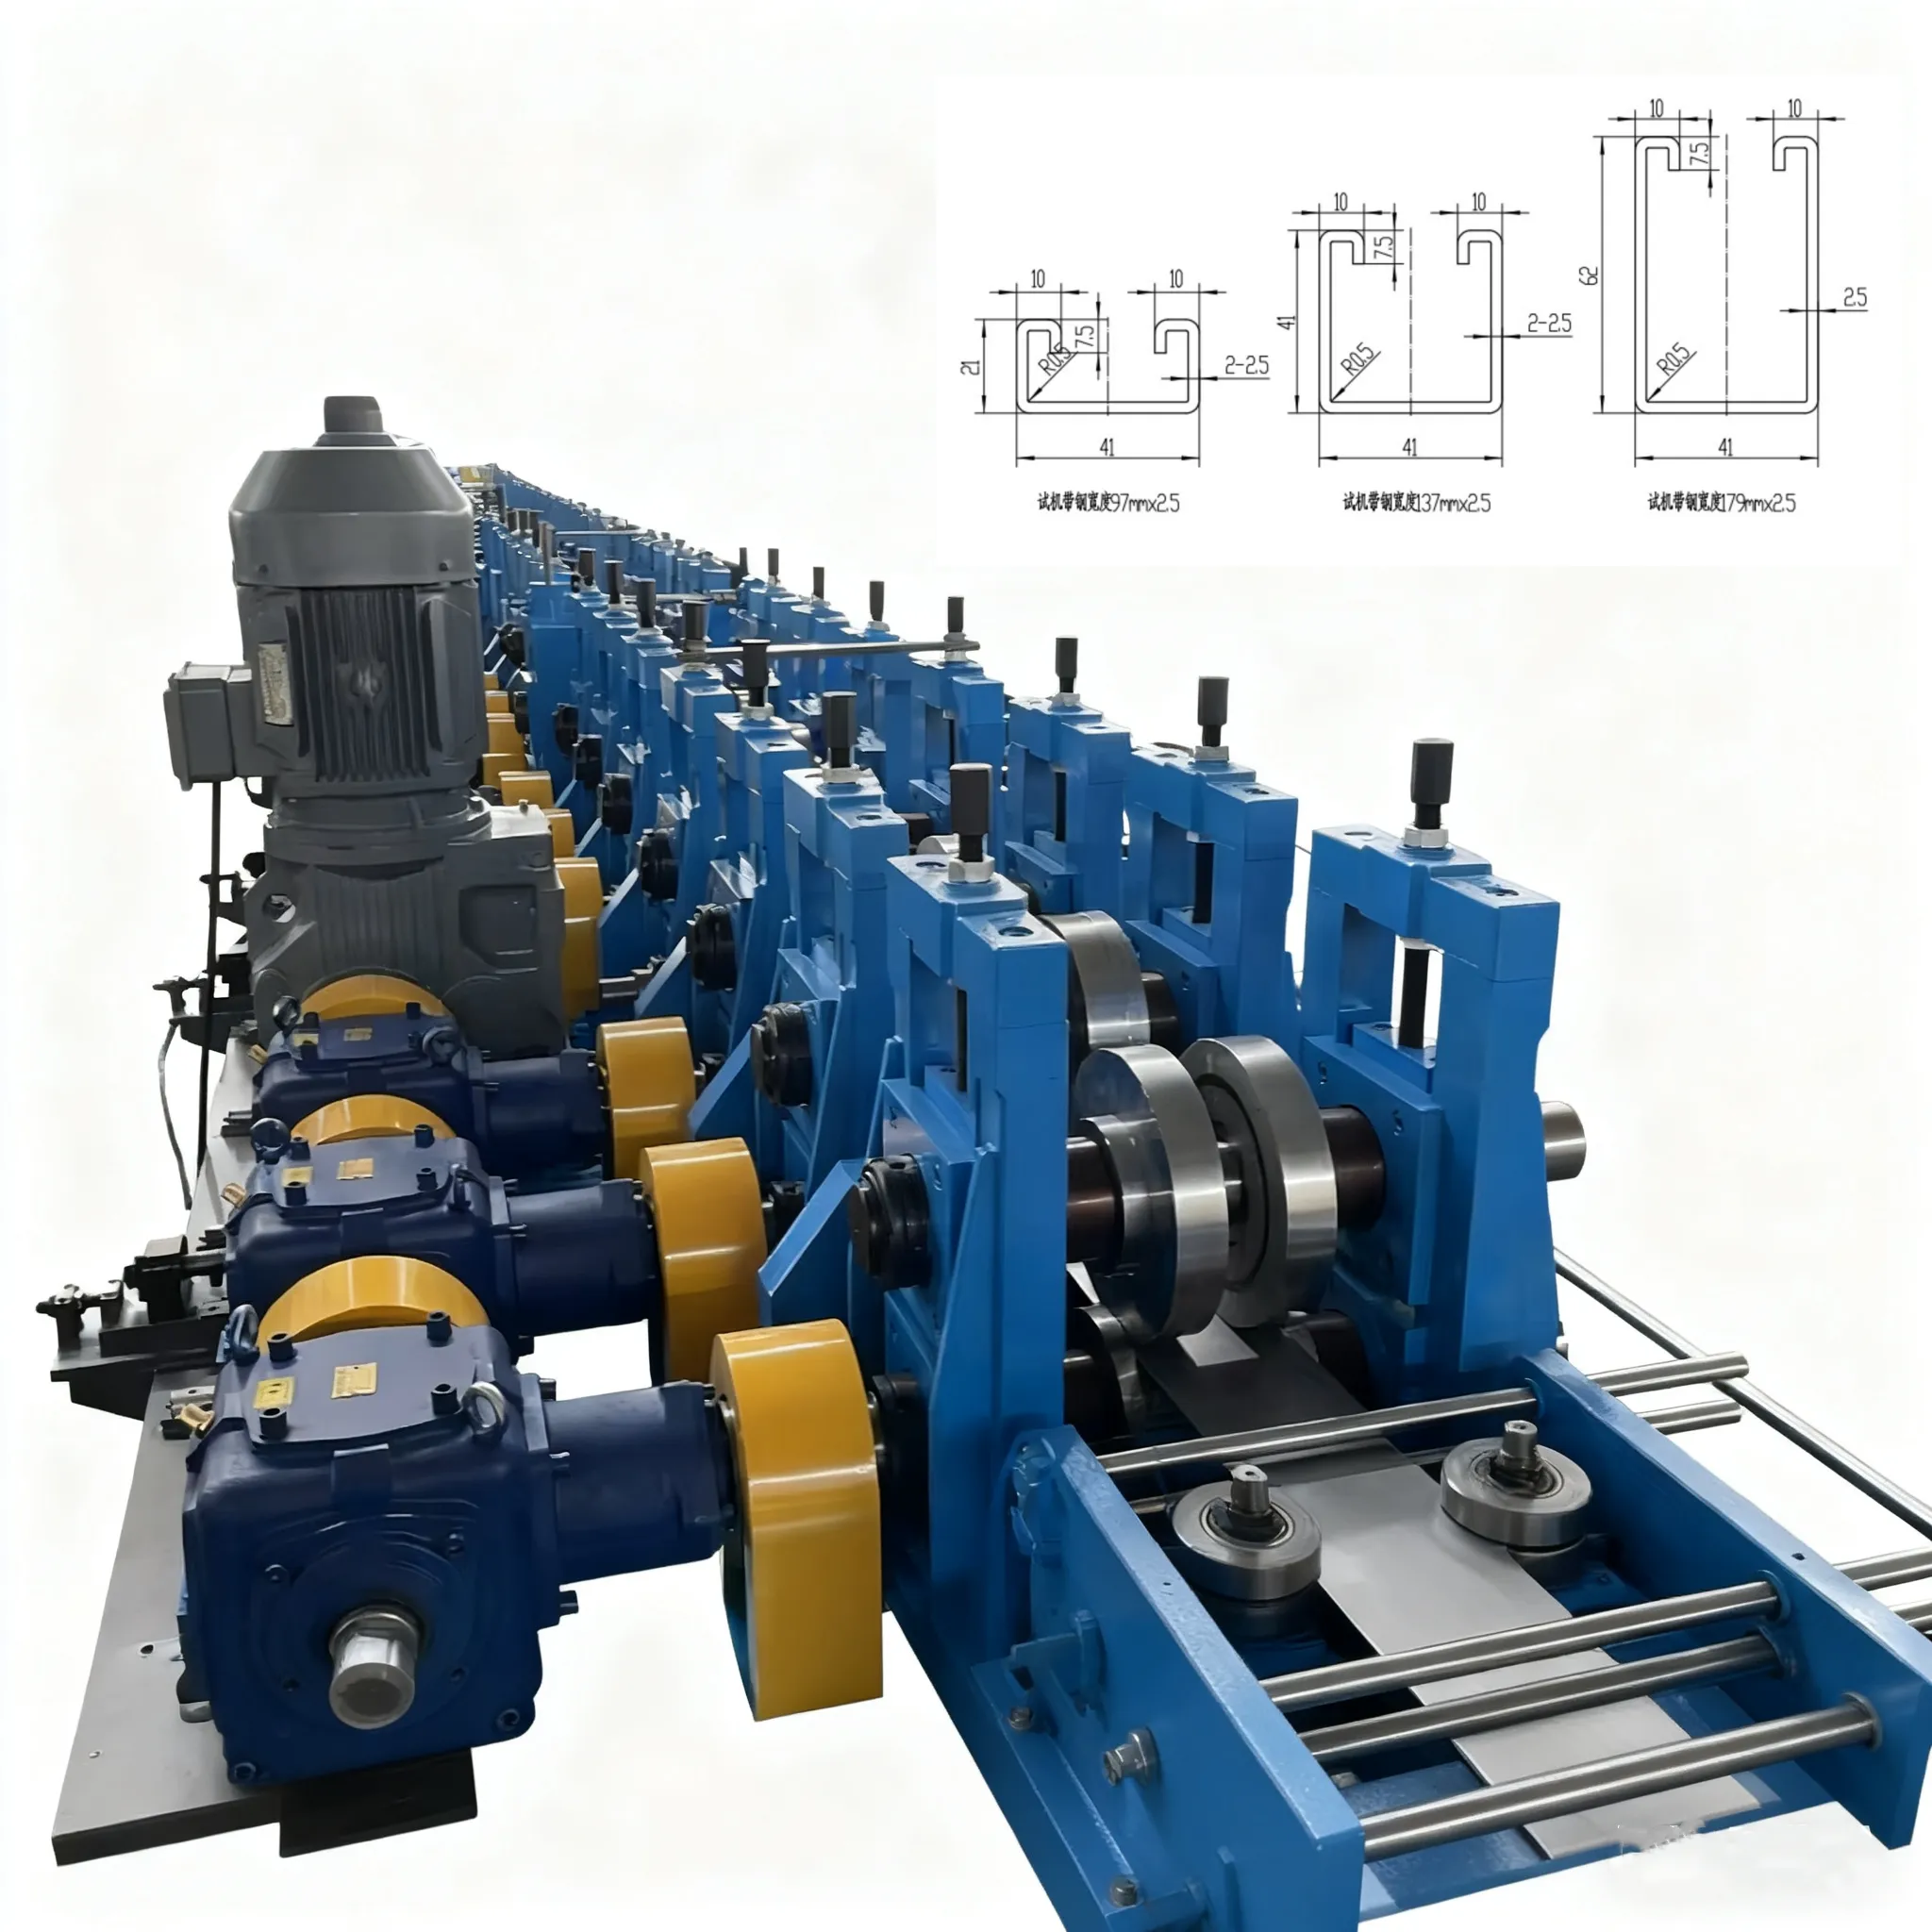 41x21 41x41 41x62 Solar Strut Channel Roll Forming Machine Solar
- 20 M/Min+ZT21-72+78kw
$102,000.00
MOQ: 1
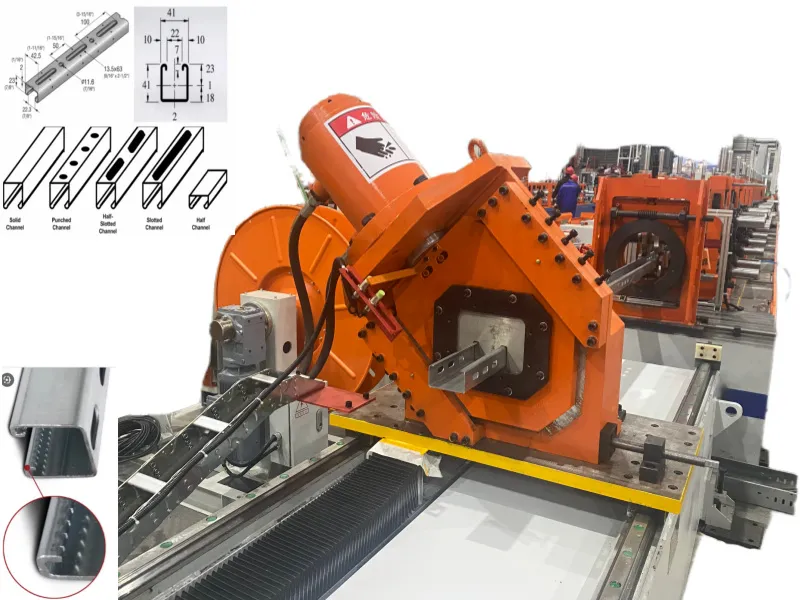 2.0-4.0 Mm CU Solar Strut Roll Forming Machine 30 M/min Unistrut
- 30 m/min+ZTRFM Solar strut roll forming machine+60-180 mm
$21,000.00
MOQ: 1
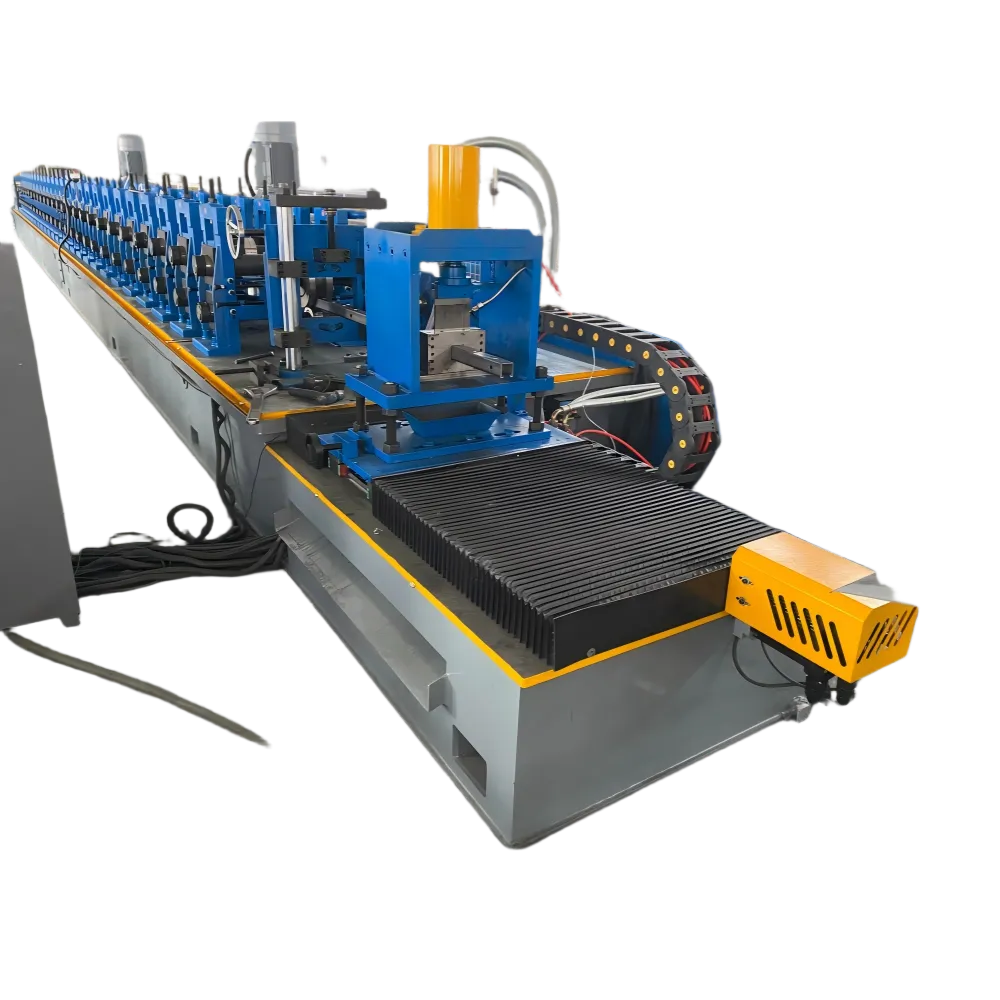 Strut Channel Solar Panel Mounting Bracket Roll Forming Machine
- 25 m/min+ZTRFM Solar Panel Bracket Roll Forming Machine+940
$11,000.00
MOQ: 1
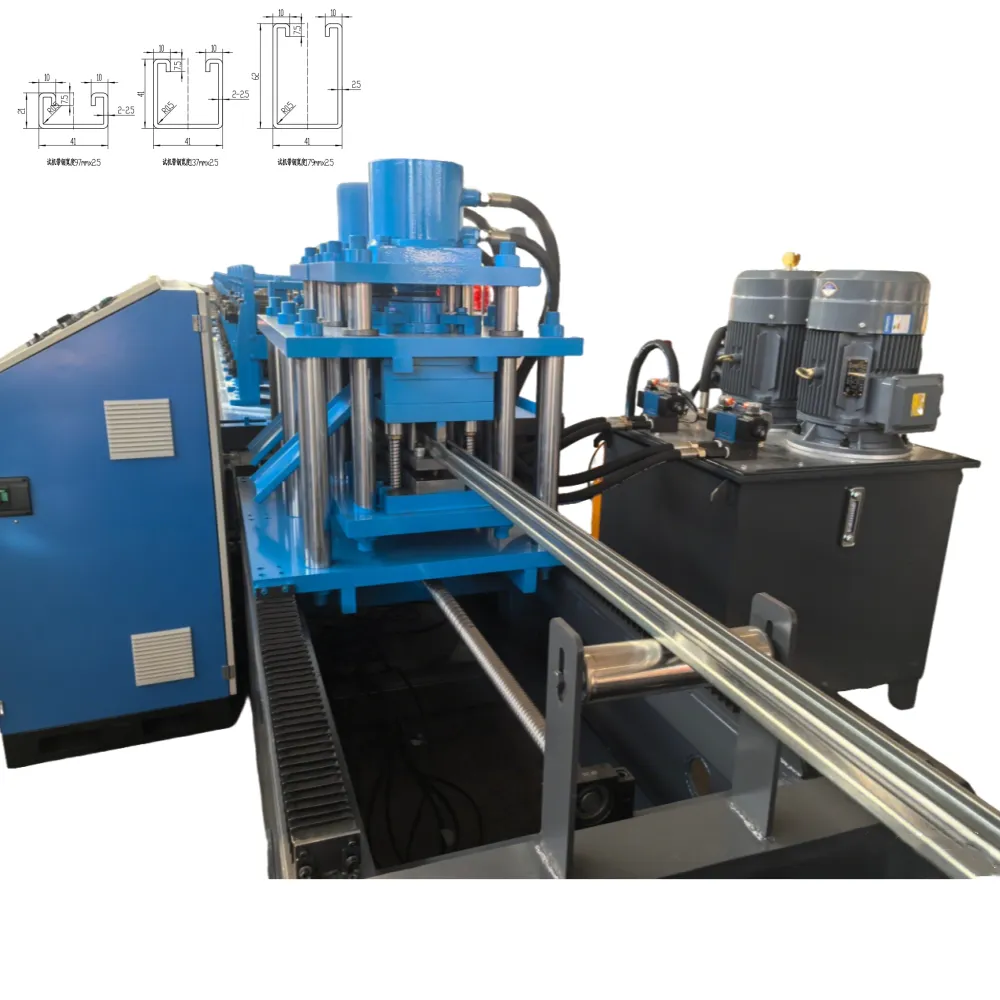 41x21 41x41 41x62 Solar Panel Mounting Roll Forming Machine Solar
- 20 M/Min+41x62+68KW
$88,000.00
MOQ: 1
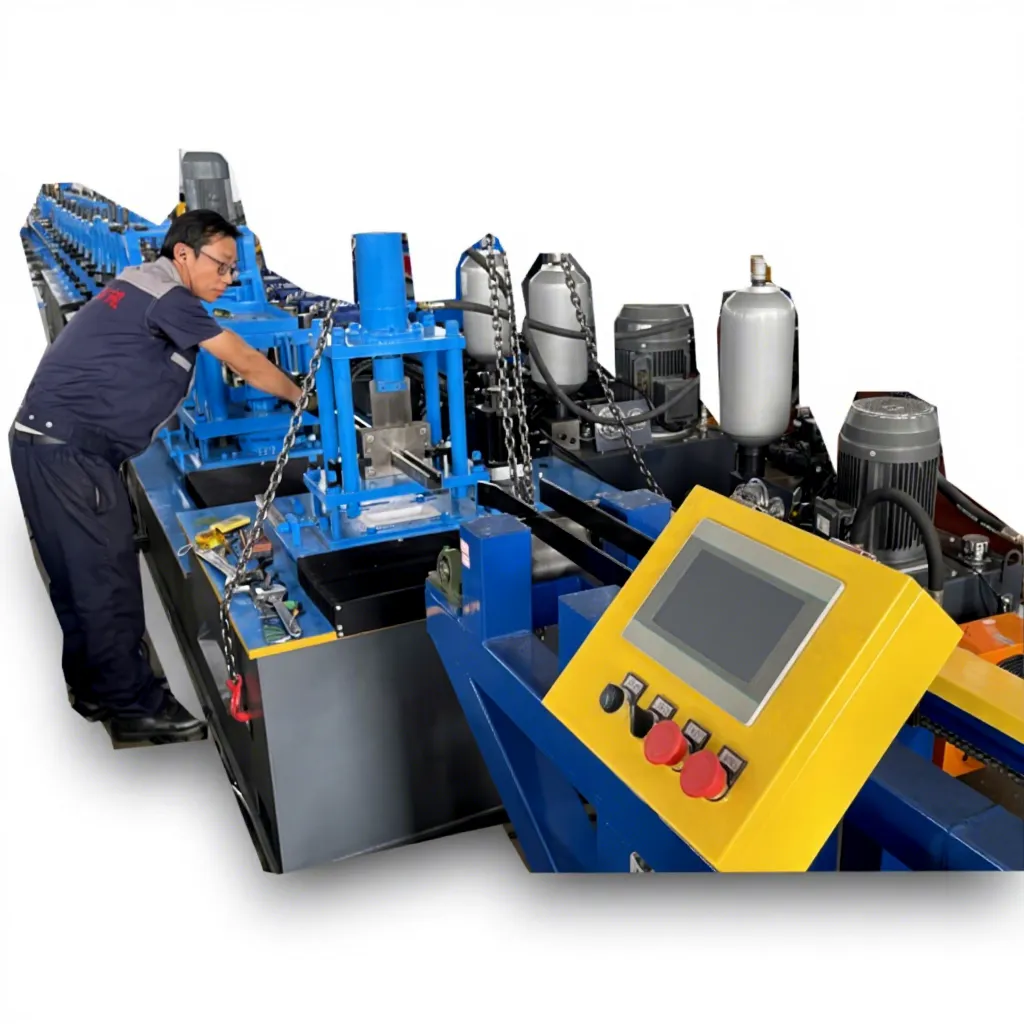 41 Solar Panel Support Purlin Roll Forming Machine 41*21 21*21
- 25 m/min+ZTRFM Solar Panel Bracket Roll Forming Machine+940
$11,000.00
MOQ: 1
 High-Precision PV Support Solar Panel Bracket Roll Forming Machine
- ZTRFM-SOLAR PANEL MACHINE
$20,000.00
MOQ: 1
 Solar Structure Channel Roll Forming Machine With Punch Press
- ZTRFM-solar panel bracket
$180,000.00
MOQ: 1
 Photovoltaic Support Roll Forming Machine for Solar Mounting System Production
- ZTRFM-solar bracket roll forming machine
$45,000.00
MOQ: 1
 Solar Panel Bracket Roll Forming Machine for PV Mounting Systems
- High Precision
$23,000.00
MOQ: 1


About Solar Panel Bracket Roll Forming Machines
Solar panel bracket roll forming machines represent essential manufacturing equipment supporting the rapid worldwide expansion of utility-scale solar photovoltaic farms, commercial rooftop solar arrays, agrivoltaic greenhouses, and solar carport structures. These specialized production lines convert structural steel coils into corrosion-resistant, high-strength mounting profiles engineered to support photovoltaic modules under severe wind-uplift pressures, heavy snow loads, and 25-plus years of outdoor exposure.
Key product profiles include standard strut channels (such as 41×41 mm, 41×21 mm, 41×62 mm) with inward return lips and optional serrated gripping teeth; heavy-gauge ground-mount post channels (C-sections, U-sections, and Omega profiles up to 120 mm web); and complex closed or open torque tube sections for single-axis tracking systems. High-performance lines increasingly process Zinc-Aluminum-Magnesium (ZAM / SuperDyma) coated steel (ZM310 to ZM430 g/m²), which provides superior self-healing corrosion protection along punched hole edges without post-forming hot-dip galvanizing baths.
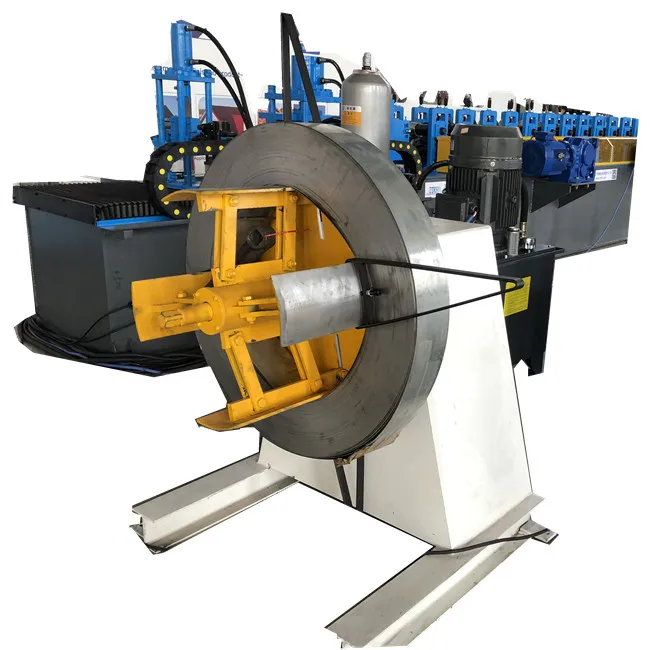
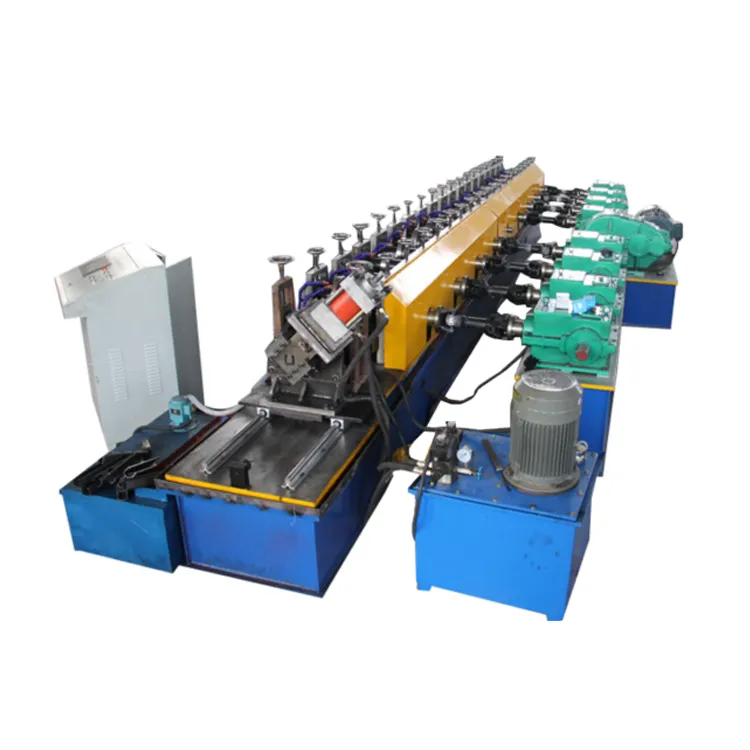
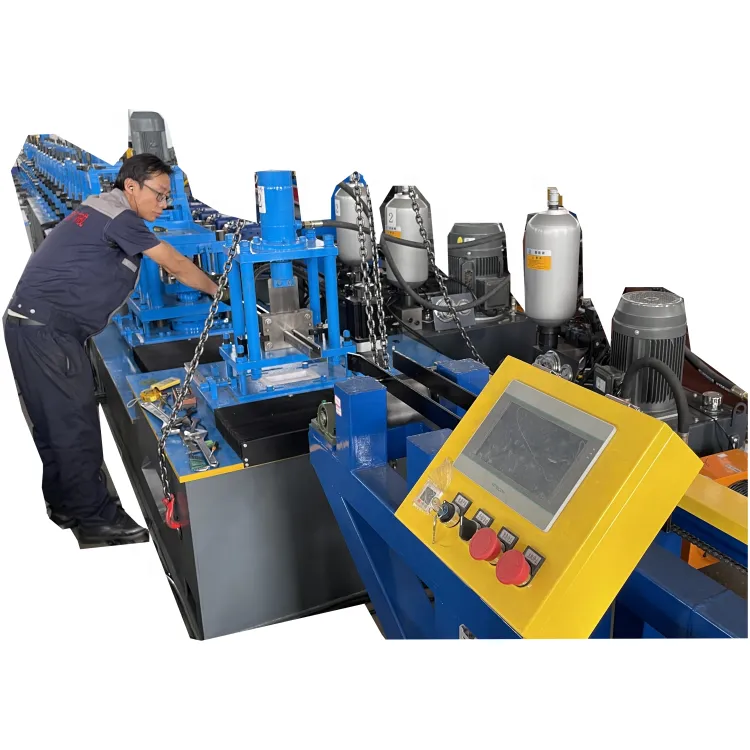
The automated manufacturing line integrates a 5-to-10-ton hydraulic decoiler with coil loading car, a 7-to-11-roll precision strip leveler to eliminate coil set, a high-tonnage servo mechanical or hydraulic pre-punching station with multi-step progressive carbide dies (capable of punching continuous slotted hole matrices at up to 100 to 150 strokes per minute), 16 to 22 heavy cast-iron roll stands utilizing solid Cr12MoV vacuum heat-treated rollers, and a high-speed servo flying cut-off saw or profile shear delivering finished line speeds of 20 to 35 m/min.
Applications
Utility-Scale Ground-Mounted Solar PV Farms
Heavy-gauge ZAM and galvanized C/U steel mounting posts and purlin brackets supporting massive multi-megawatt desert and plains solar photovoltaic panel arrays.
Commercial & Industrial Rooftop Solar Racking
Cold-formed 41×41 mm strut channels and ballast mounting rails fixing commercial rooftop solar arrays onto industrial standing seam metal roofs with zero roof penetrations.
Agrivoltaic Farm Greenhouse Solar Structures
Elevated galvanized steel bracket posts and mounting purlins supporting solar panel canopies above agricultural crop fields and automated greenhouse complexes.
Solar Carport & EV Charging Canopy Structures
Heavy cantilevered roll-formed steel bracket beams and solar rails forming commercial parking canopies integrated with electric vehicle charging stations.
Floating Solar PV Mounting Platforms
Highly corrosion-resistant aluminum and ZAM roll-formed mounting brackets securing photovoltaic panels onto HDPE floating pontoons across water reservoirs and lakes.
Technical Overview
| Parameter | Information |
|---|---|
| Machine / Product Family | Solar photovoltaic mounting bracket & strut channel roll forming line |
| Applicable Coil Materials | Hot-dip galvanized steel (GI), Zinc-Aluminum-Magnesium (ZAM / SuperDyma) |
| Material Thickness Range | 1.50 mm – 3.00 mm (16-gauge to 11-gauge structural strip) |
| Steel Yield Strength Range | S350GD+Z/ZM to S550GD+Z/ZM (350 MPa to 550 MPa yield) |
| Standard Profile Models | 41×41 mm, 41×21 mm, 41×62 mm strut channels & custom C/U ground posts |
| Punching System & Speed | High-tonnage servo mechanical/hydraulic punch; 80 – 120 strokes/min |
| Forming Stations & Tooling | 16 – 22 heavy-duty cast-iron stands (solid Cr12MoV rollers, HRC 60–62) |
| Lip Serration Feature | Integrated auxiliary knurling wheels for slip-resistant channel nut teeth |
| Cutting System & Tolerances | Synchronized servo flying cut-off (Cr12MoV); length tolerance ±1.0 mm |
| Line Speed & Capacity | 20 – 35 m/min production speed; daily capacity 15 – 25 metric tons |
Related Solutions
Solar Mounting Roll Forming Solution
Solar strut / hat-bracket mill for PV mounting. Example: 24 stands with cooling,…
Custom Profile Roll Forming for OEM
Flexible roll forming line for custom cross-sections. Suitable for OEMs who need…
Pre-Engineered Building Component Line
Integrated solution for PEB secondary framing: C/Z purlins, girts, eave struts,…
Roof & Wall Purlin System Solution
Secondary steel for roofs and walls is a section family first: dedicated C, dedi…
Heavy Coil Handling Solution
Coil infeed is a weight class plus a drive: manual expand, electric expand with…
Metal Sheet Processing Solution
Blanking and cut-off around a roll former is a shear class: flying (tracking) sh…
Related Information

Solar Mounting Structures: Roll-Formed Racking That Lasts 25 Years
Every solar farm stands on roll-formed C, U and Omega sections. Why Zn-Al-Mg coa…
Read More
Solar Strut Channel Roll Forming Line: Profiles, Specs & What to Buy
solar strut channel roll forming line, solar mounting bracket roll forming machi…
Read More
What Is a Solar Strut Channel Roll Forming Machine? Components, Profiles & Specs
solar strut channel roll forming machine
Read More
Solar Tracker Bracket Roll Forming Machines: Forming Zinc-Aluminum-Magnesium (ZAM) Steel Profiles
solar strut channel machine, ZAM steel roll forming, zinc aluminum magnesium rol…
Read More
Cold Formed Steel vs Hot Rolled Steel: What Roll Forming Buyers Need to Know
Yield strength, ductility, surface finish, tolerances — a practical comparison o…
Read More
High-Strength Steel (HSLA) in Roll Forming
High-strength low-alloy steel lets you build lighter structures—but it fights ba…
Read More
FAQ
What profile types can be manufactured on a solar panel bracket roll forming machine?
Machines produce standard strut channels (41×41 mm, 41×21 mm, 41×62 mm), C-channels, U-channels, hat sections (Omega profiles), and heavy ground-mount pile posts. With interchangeable cassette tooling, one machine base can produce multiple mounting profiles.
Why is Zinc-Aluminum-Magnesium (ZAM) steel coil widely used in solar bracket roll forming?
ZAM steel features an alloy coating of zinc, aluminum, and magnesium that provides 3 to 5 times higher corrosion resistance than traditional galvanized steel. The magnesium creates a protective sacrificial zinc-hydroxide film that flows over and self-heals sheared cut edges and punched holes, eliminating secondary post-galvanizing dips.
What material thickness and steel grades can solar bracket roll forming lines handle?
Standard lines process material thicknesses from 1.5 mm to 3.0 mm (16-gauge to 11-gauge). Structural steel grades typically range from S350GD+ZM to S550GD+ZM (yield strength 350 to 550 MPa) to ensure rigid wind resistance.
How is continuous high-density hole punching achieved without slowing down forming speed?
High-output lines utilize high-tonnage servo mechanical or hydraulic punching presses equipped with multi-cavity progressive carbide die sets. A servo feeder advances strip in micro-steps, punching multiple slotted holes per stroke at rates up to 120 strokes/min before the strip enters forming rolls.
Can solar strut channels be formed with inward serrated teeth along the return lips?
Yes. Advanced tooling incorporates auxiliary knurling and serrating wheels on early forming stations that coin sharp, hardened grip teeth along the inward lips. These teeth bite into spring channel nuts, preventing module slippage under dynamic wind vibration.
Stop-to-cut vs. servo flying cut-off: which shear system is recommended for solar brackets?
Servo flying shear is strongly recommended for high-volume solar production. It cuts moving channels at speeds up to 25–35 m/min without stopping the mill, ensuring high daily tonnage and preventing tool jamming on punched hole patterns.
What parameters should buyers verify when sourcing a solar bracket roll forming machine?
Buyers should confirm channel profile drawings (lip depth, web width, serration details), maximum thickness (up to 2.5 or 3.0 mm), punch die hole tolerances (±0.5 mm hole center pitch), roller material (Cr12MoV vacuum hardened to HRC 60), and flying cut-off drive power.