
- Tuo AI

- Live

- My Account
- Shopping Cart
- Inquiry Basket
- Contact Us
- Back to Top




Purlin Roll Forming Machines
Purlin roll forming machines continuously produce cold-formed structural C and Z secondary framing members for industrial pre-engineered steel buildings, logistics warehouses, and solar mounting structures. Engineered to process high-yield galvanized steel coils (S350GD to S550GD, 1.5 mm to 3.5 mm thick), modern automatic CZ quick-change lines adjust web depths (80 mm to 300 mm), flange widths, and return lips in minutes via touchscreen PLC commands. Featuring multi-cylinder hydraulic punching for precision bolt slots and universal stepless hydraulic or flying shears, these lines deliver exceptional structural straightness and high throughput. Explore verified machine specifications, tooling configurations, and factory-direct solutions below.
Filters
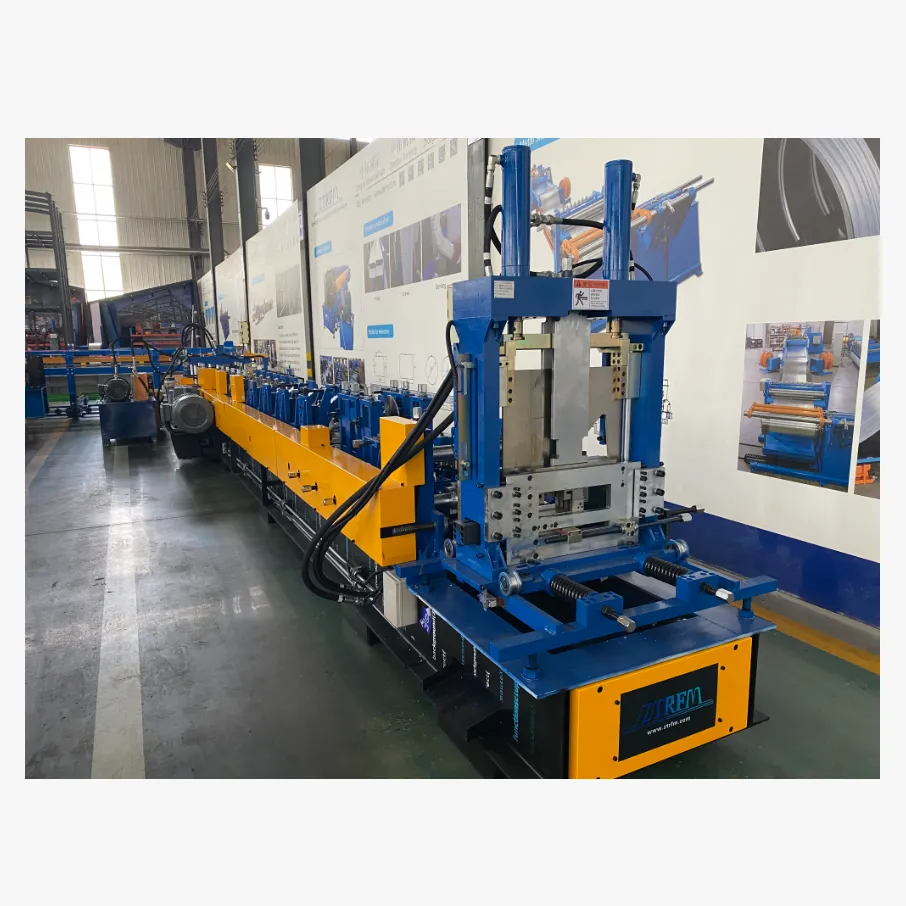 250 C Purlin Profile Roll Forming Machine Colored Core Components
- 25 M/min+CZ PURLIN ROLL FORMING MACHINE+14KW+7.5KW
$31,000.00
MOQ: 1
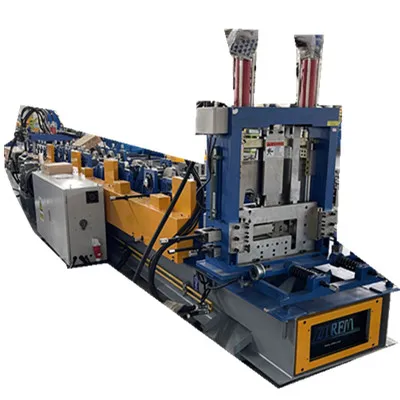 Steel 40-350 C/Z Changeover Roll Forming Machine
- 20m/ min+zt300+400
$1.00
MOQ: 1
 Intelligent Visualization Roof Tile Forming Machine Servo Drive
- 30 m/min+30KW (WK series Hydraulic motor)
$50,000.00
MOQ: 1
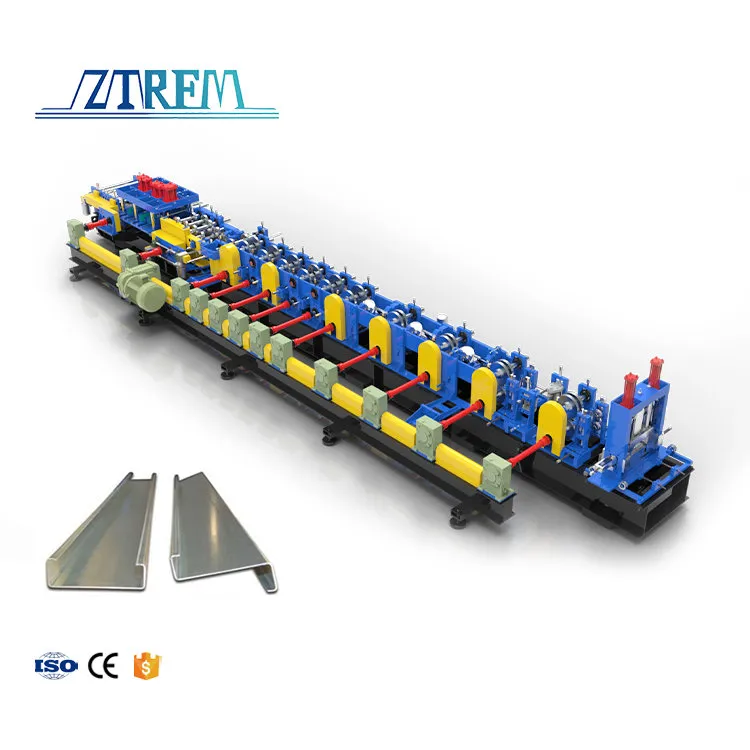 8 Inch Cee Zee Home Frame Making Machine
- 37m/min+Purlin -002+500mm
$50,000.00
MOQ: 1
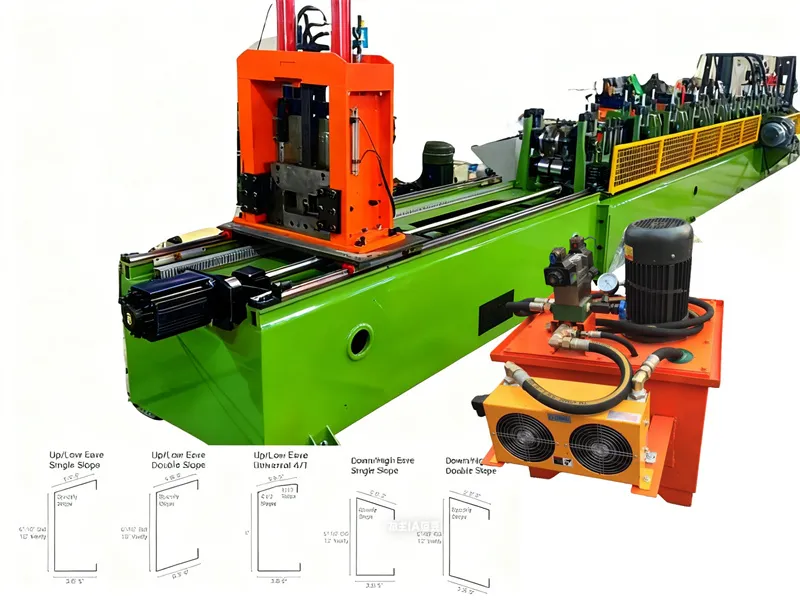 1.9-2.6mm Eave Strut Roll Forming Machine 8 10 & Inch
- 10-15 m/min+ZTRFM Eave Strut Roll Forming Machine+7inch, 8inch, 10inch
$20,000.00
MOQ: 1
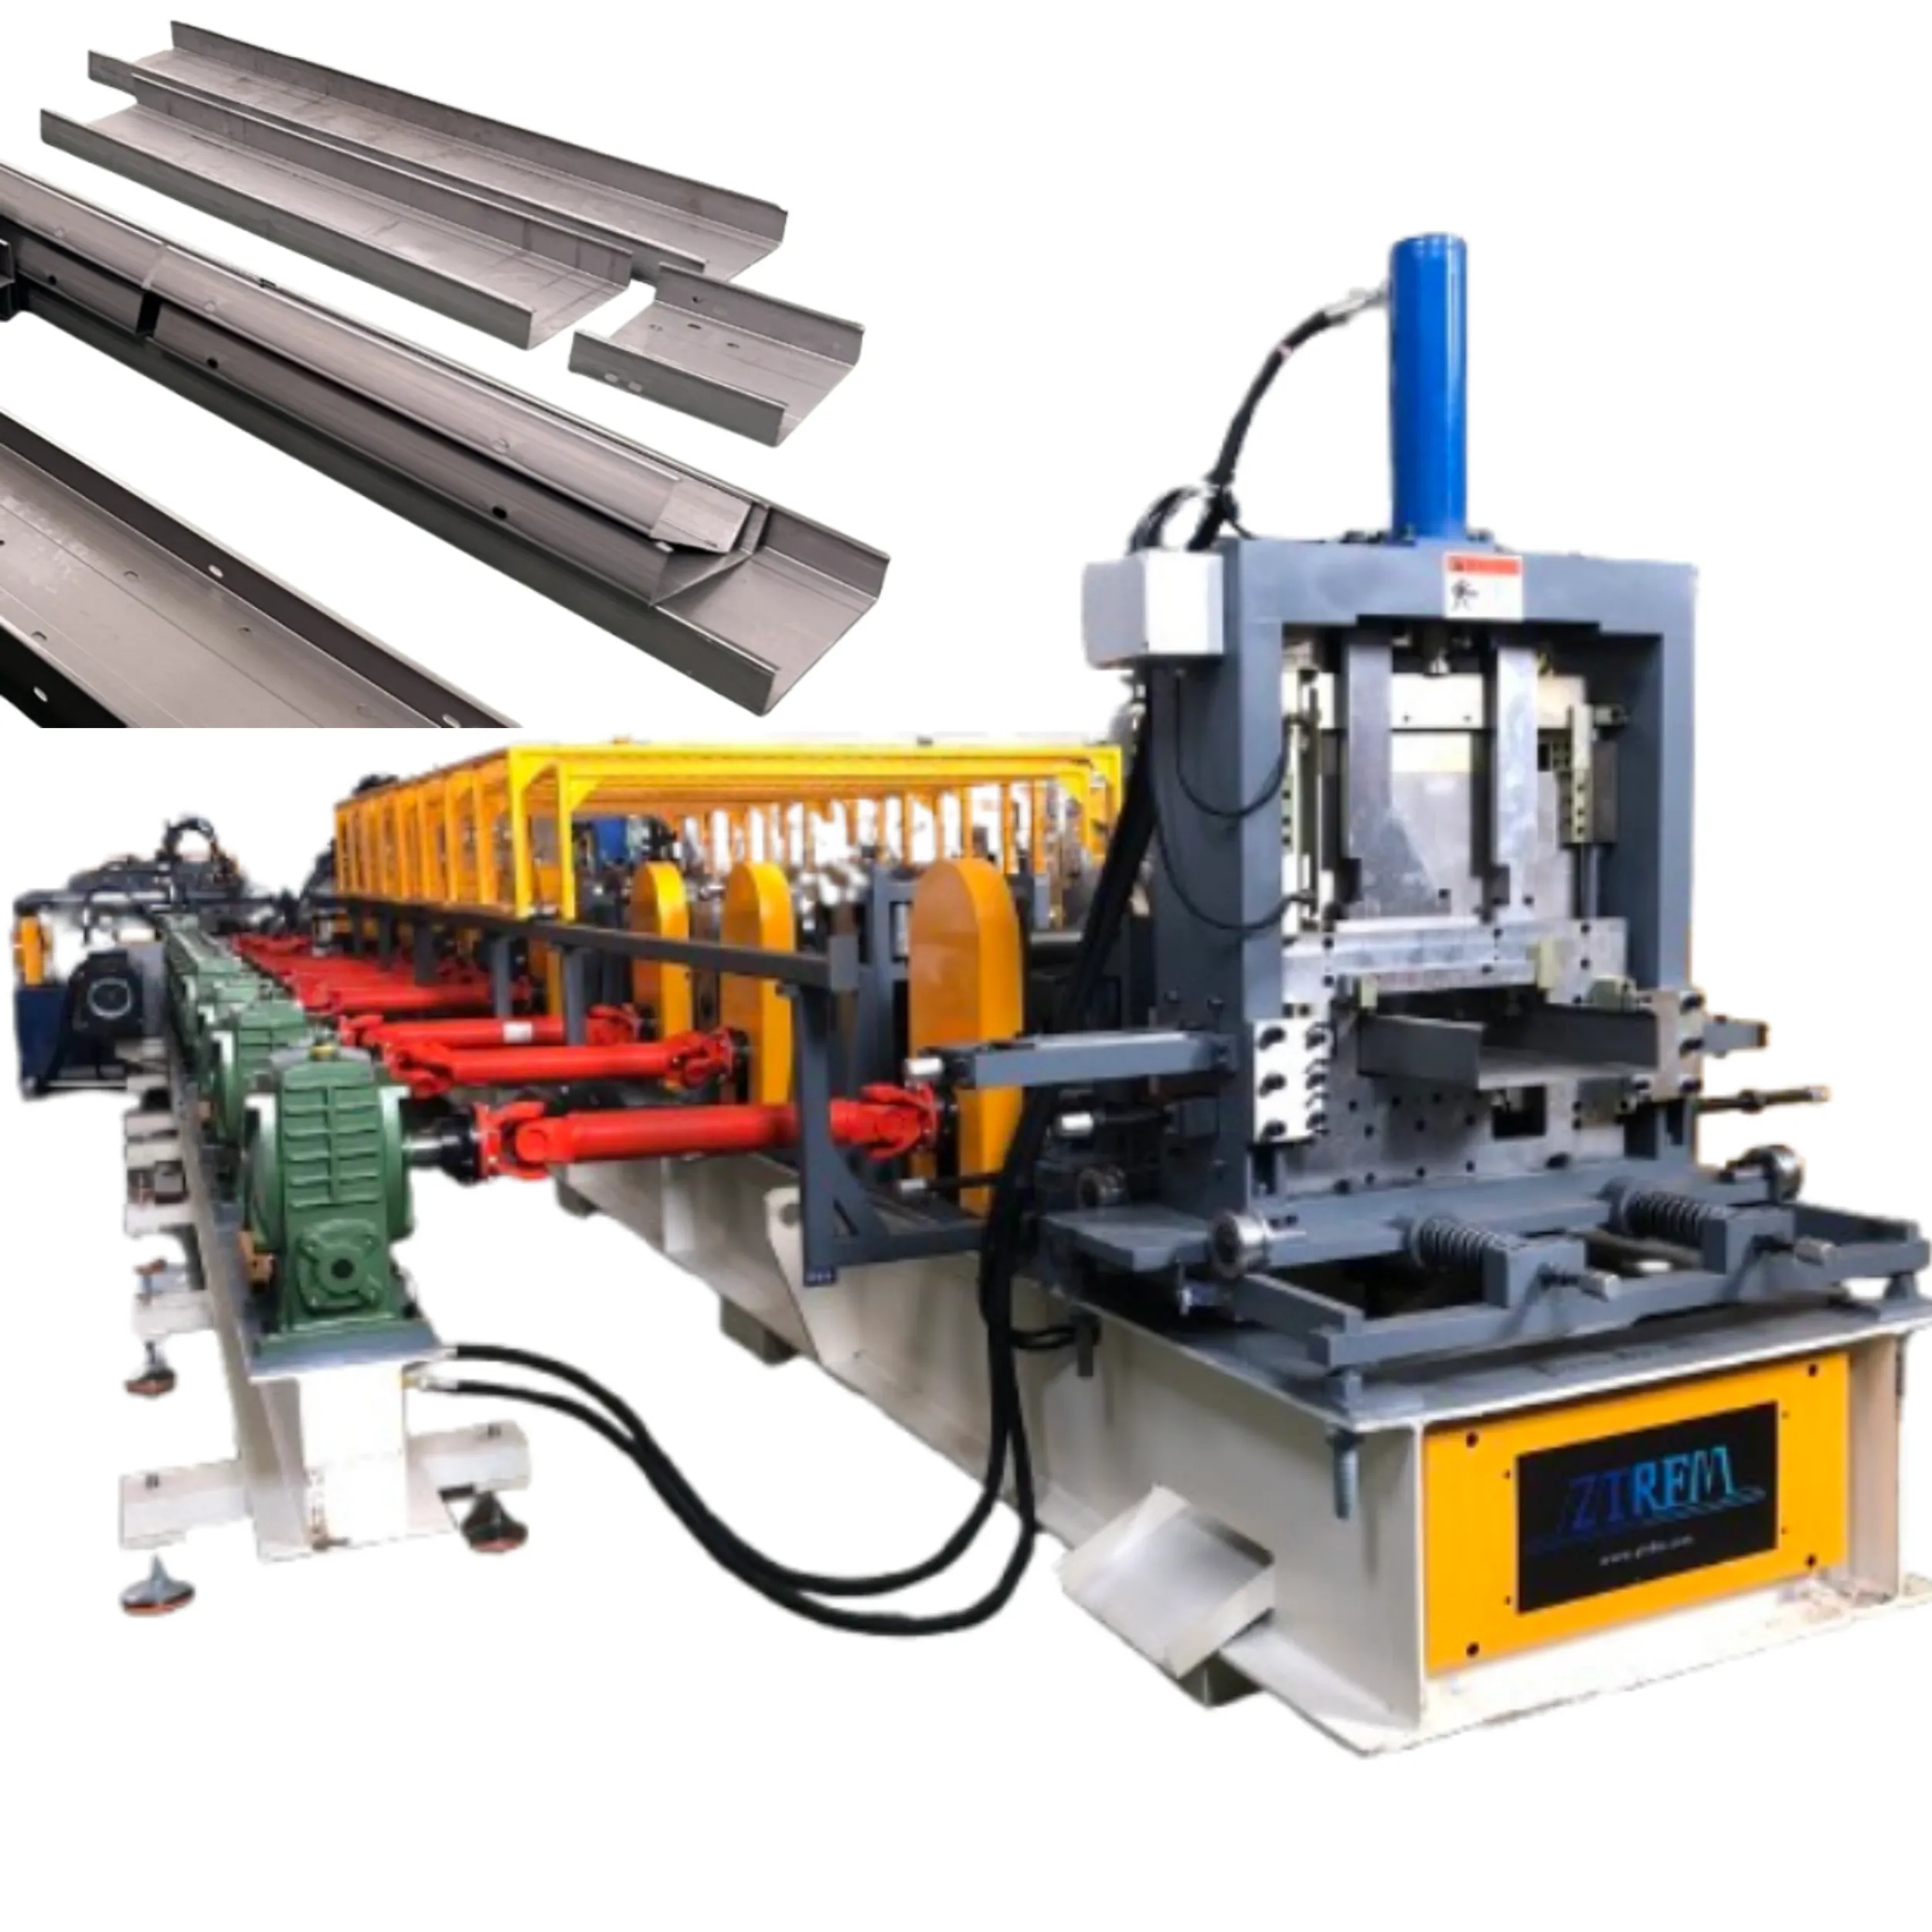 Steel CZ Frame & Purlin & Cutting System
- 40m/min+CZ Steel Frame & Purlin Machines+400
$25,000.00
MOQ: 1
 Interchangeable CZ Purlin Roll Forming Machine
- 37m/min+Purlin -003+500mm
$42,000.00
MOQ: 1
 Precision Heavy Gauge CZ Purlin Roll Forming Machine Box
- 20m/ min+zt300+400
$50,000.00
MOQ: 1
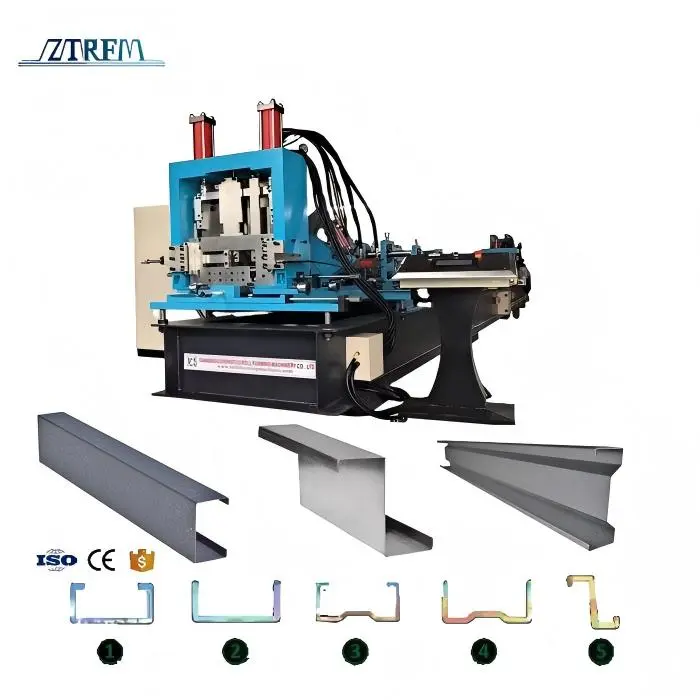 C U Profile Sigma M Purlin Roll Forming Machine Steel Frame
- ZTRFM Eave Strut Roll Forming Machine+7inch, 8inch, 10inch+10m/min
$20,000.00
MOQ: 1
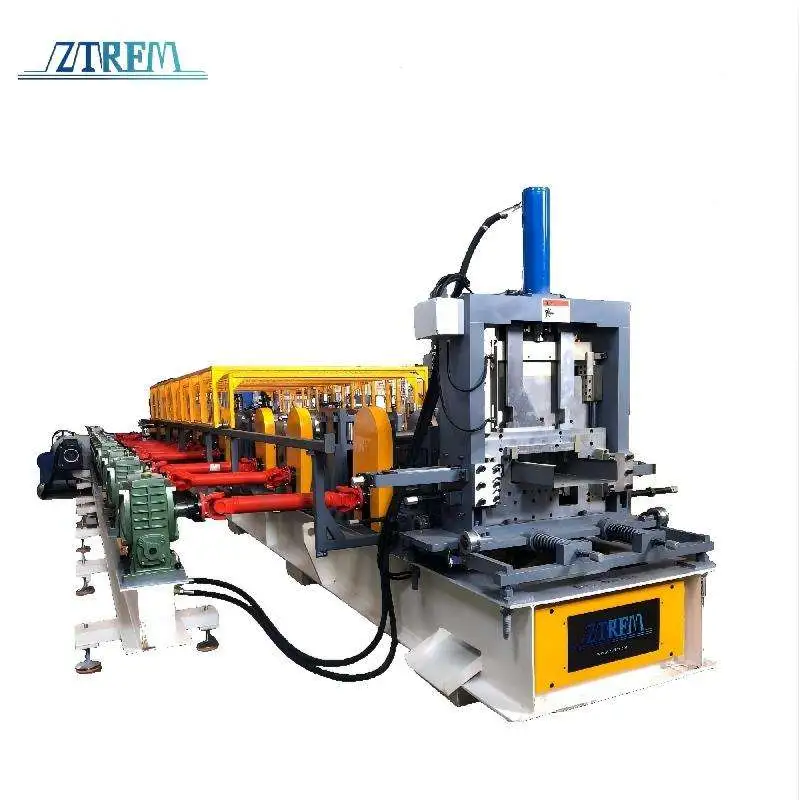 Sigma Section Purlin Roll Forming Machine M Channel Purline
- ZTRFM Eave Strut Roll Forming Machine+7inch, 8inch, 10inch+10m/min
$19,000.00
MOQ: 1
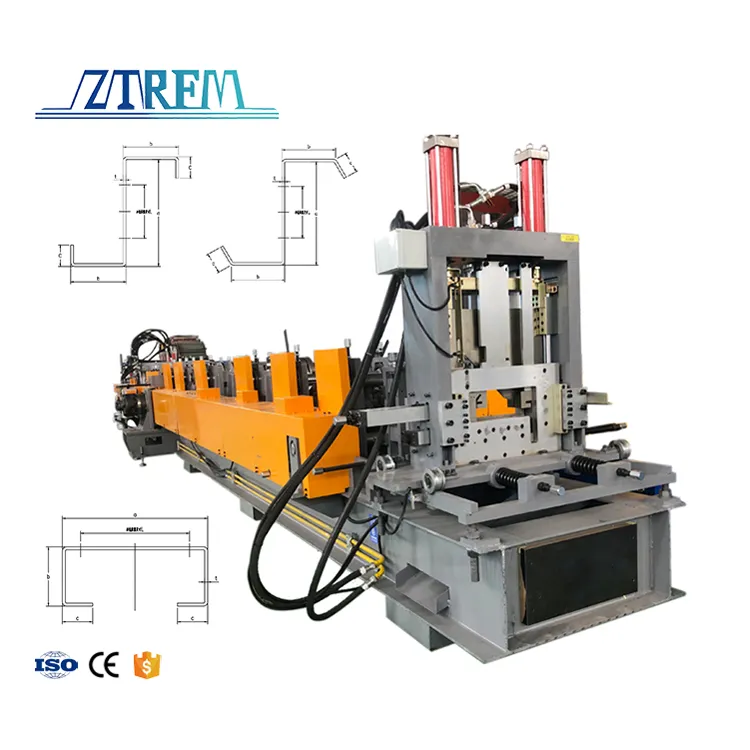 Power System Changing Sizes America Area CZ Purlin Machine
- 37m/min+Purlin -002+500mm
$50,000.00
MOQ: 1
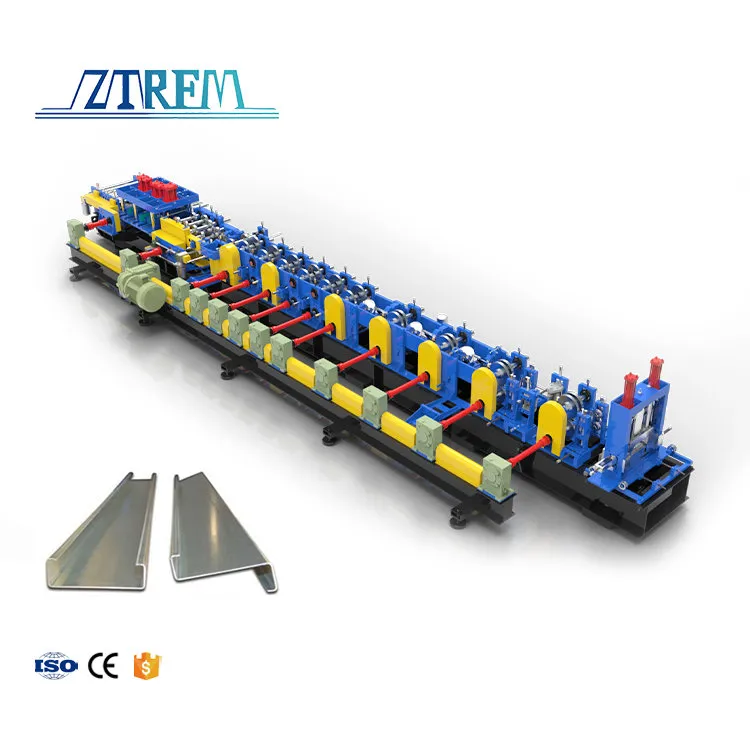 4 Inch Zee 6 Inch Cee 14 Gauge Steel Frame Roll Forming Machine
- 30m/min+CUZ+customized
$50,000.00
MOQ: 1
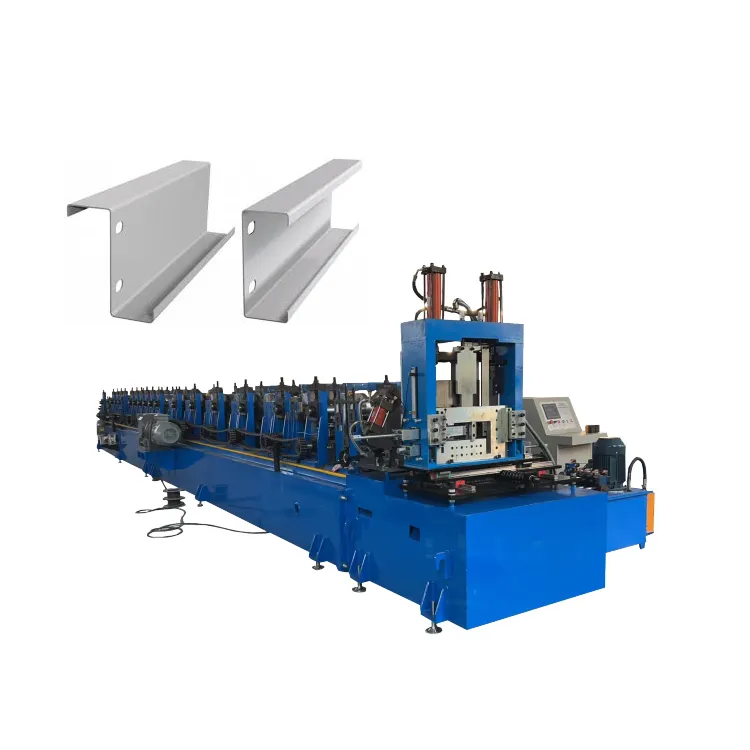 CZ Purlin Roll Forming Machine System Design
- 37m/min+Purlin -002+500mm
$50,000.00
MOQ: 1
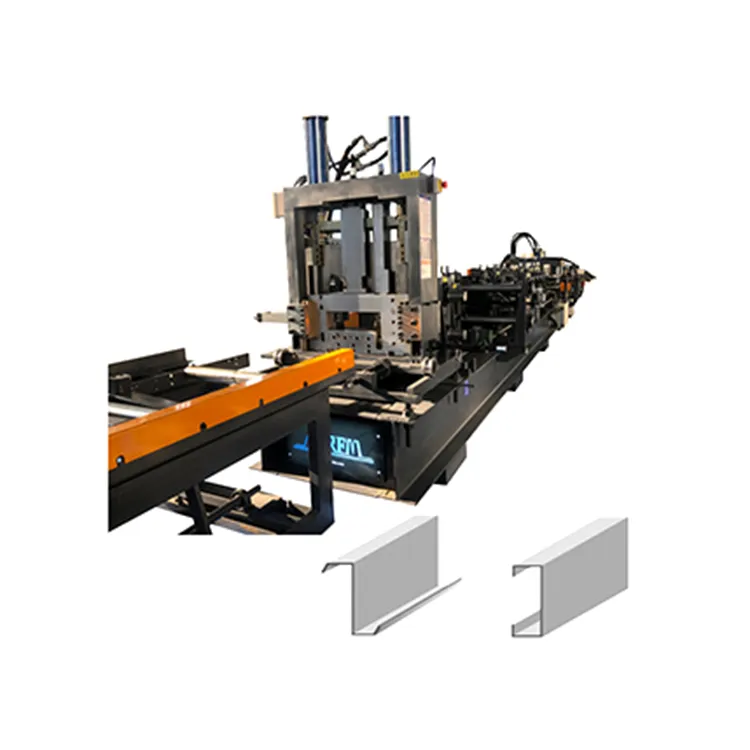 Servo Drive C Z Us Area Purlin Roll Forming Machine Metal Frame
- 37m/min+Purlin -002+500mm
$50,000.00
MOQ: 1
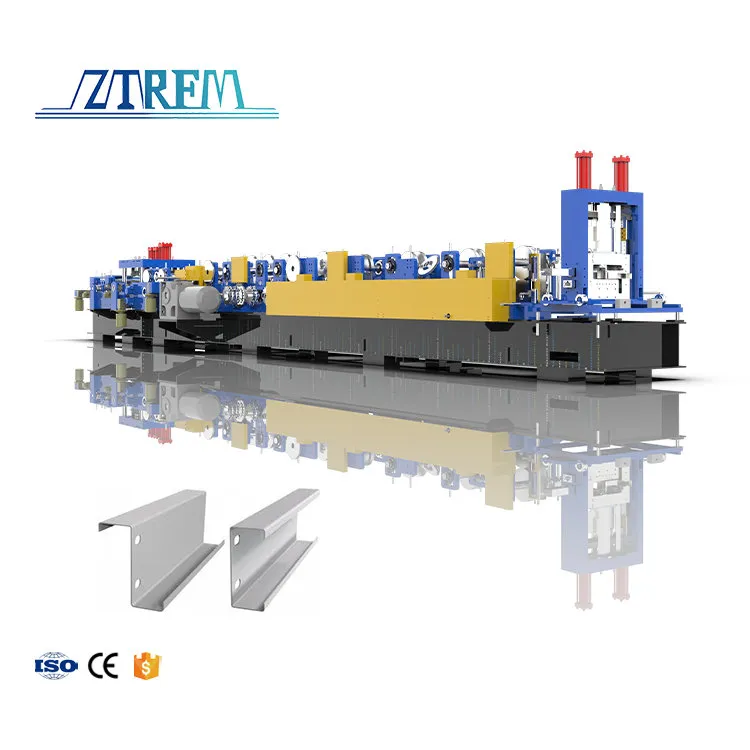 US Area Zee Purlin Roll Forming Machine 4 6 Inch Cee Purlin
- 37m/min+Purlin -002+500mm
$35,000.00
MOQ: 1
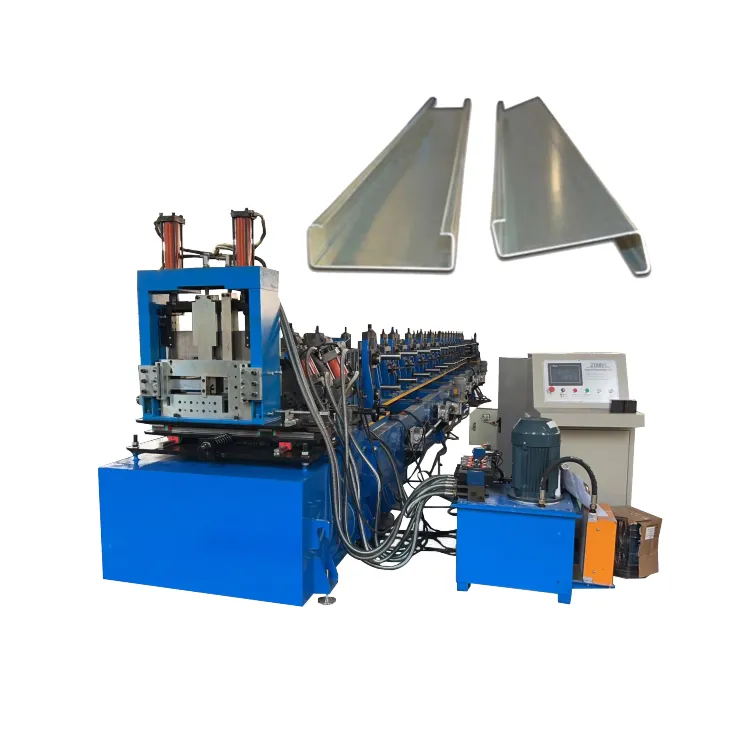 CZ Purlin Roll Forming Machine & Components
- 37m/min+Purlin -002+500mm
$50,000.00
MOQ: 1
 America Area CZ Purlin Machine Steel Frame Make Machine Power
- Purlin -002+500mm
$50,000.00
MOQ: 1
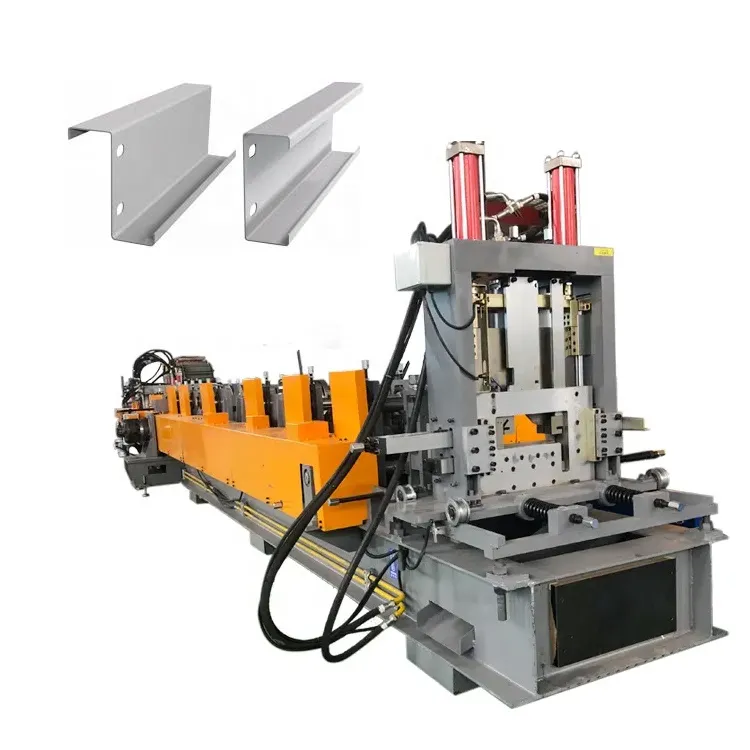 Support Sizes Shape Changing C Z Purlin Roll Forming Machine
- Purlin Machine-001+500mm
$50,000.00
MOQ: 1
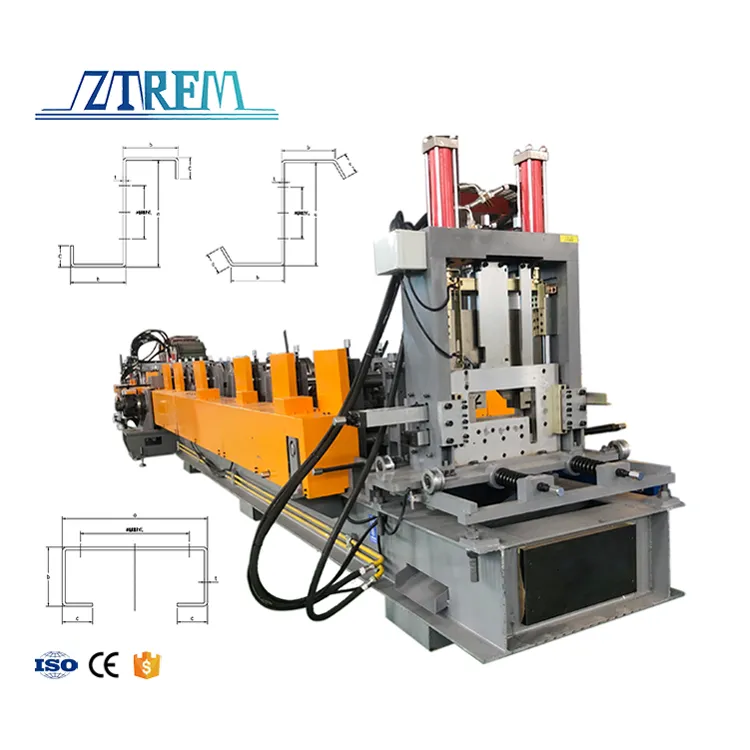 Product C Z Purlin Roll Forming Machine
- 30 m/min+C Z Purlin Machine+30KW (WK series Hydraulic motor)
$50,000.00
MOQ: 1
 C Z Purlin Roll Forming Machine Steel & Frame
- 37m/min+Purlin -004+500mm
$50,000.00
MOQ: 1
 8 Inch Cee Zee Home Frame Making Machine
- Purlin -002+500mm
$50,000.00
MOQ: 1
 C Z Purlin Roll Forming Machine 200-600 Sigma
- 30m/min+CUZ+customized
$40,000.00
MOQ: 1
 Steel Muti Functional Tile Making C Z U Frame Purlin
- 37m/min+Purlin -002+500mm
$50,000.00
MOQ: 1
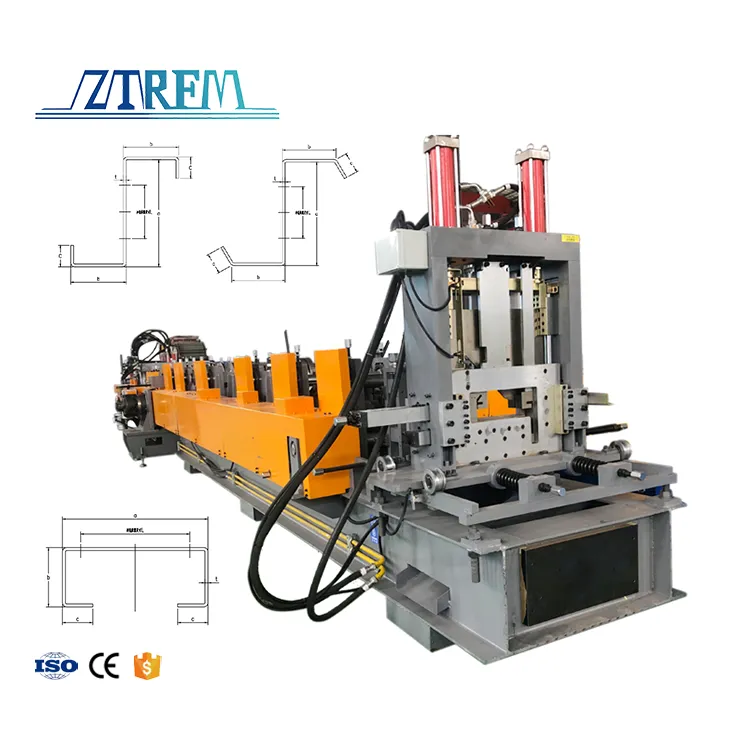 C Z Purlin Roll Forming Machine China CZ Purline Roll Forming Machine
- 30 m/min+ZTRFM-C11+30KW (WK series Hydraulic motor)
$50,000.00
MOQ: 1
 C Z Purlin Roll Forming Machine C Z Purlin Machine CZ Roll
- 37m/min+Purlin -004+500mm
$50,000.00
MOQ: 1
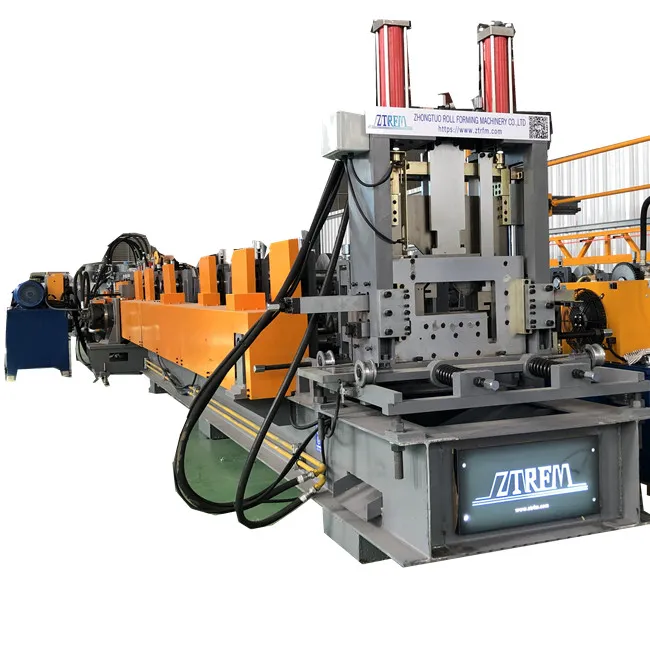 Cee Zee M Purlin Profile C Z Purlin Roll Forming Machine
- 5 m/min+18.5kw
$60,000.00
MOQ: 1
About Purlin Roll Forming Machines
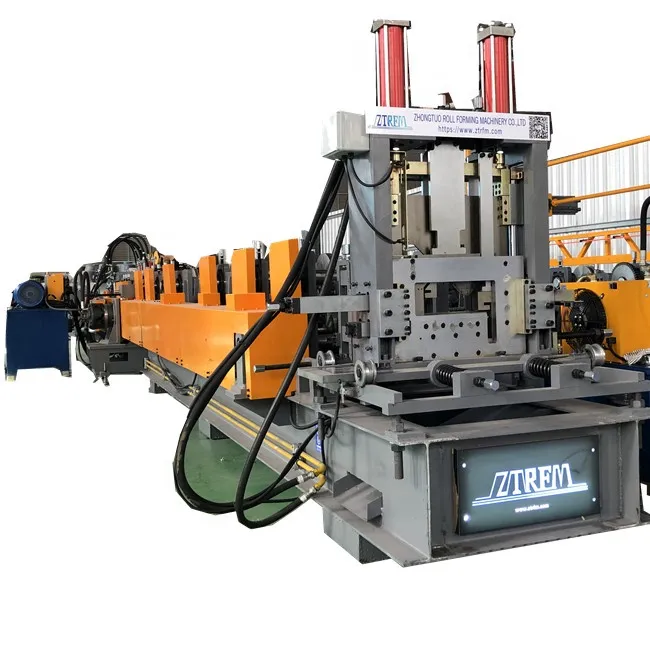
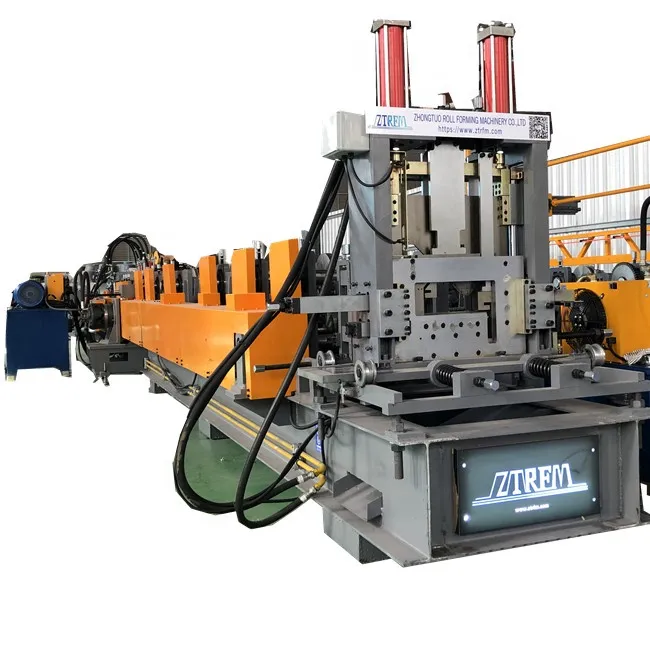
Purlin roll forming machines represent core capital equipment in structural steel manufacturing, pre-engineered building (PEB) fabrication, and solar racking infrastructure. Unlike fixed-profile roll formers, automated CZ purlin machines offer flexible dimensional adjustment across dozens of standard C-channel and Z-section profiles (C80–C300 and Z100–Z300) on a single compact chassis, eliminating costly and time-consuming manual roller disassembly.
Modern quick-change lines feature computer-controlled motorized width adjustment driven by high-torque servo motors and precision ball screws. Web height (80 mm to 300 mm), flange width (40 mm to 80 mm), and lip angle are adjusted synchronously within 2 to 5 minutes through the central HMI touchscreen. Profile changeover between C-purlin and Z-purlin is achieved either by rotating forming roller cassettes 180 degrees or through automated motorized shifting stations, dramatically reducing changeover downtime in high-mix job-shop environments.
The typical production line integrates a 5-to-10-ton hydraulic uncoiler with loading car, precision 7-roll sheet leveler, multi-cylinder hydraulic pre-punching station for round and slotted cleat bolt holes (with web and flange hole spacing programmed via CNC), 14 to 18 heavy-duty forming stations utilizing solid GCr15 or Cr12MoV vacuum heat-treated rollers (HRC 58–62), and an intelligent universal hydraulic cut-off unit that shears all C and Z profile dimensions without blade replacement at speeds up to 25 to 35 m/min.
Purlin Roll Forming Machines Profiles

C100×50×15
Structural C purlin example; typical line range 1.0–3.0 mm on C80-300 class host…
View Profile

Z200×70×20
Z purlin uses a different roll set from C — not interchangeable on the same host…
View Profile
C80–300 adjustable range
Automatic C80-300 host class; 1.0–3.0 mm typical on recommended offer.
View Profile
Applications
Pre-Engineered Steel Building Roof & Wall Purlins
Continuous overlapping galvanized Z-purlins and C-wall girts roll formed for large pre-engineered steel buildings, supporting roof panels and heavy mechanical services.
Heavy-Duty Industrial Crane Workshop Framing
Heavy-gauge C-purlins (250 mm to 300 mm web) bolted horizontally between vertical H-columns in manufacturing plants, supporting side cladding and crane runways.
Commercial Logistics Center Continuous Z-Purlins
High-tensile continuous Z-purlin secondary framing systems engineered for expansive commercial logistics fulfillment centers requiring long clear rafter spans.
Solar Ground Mounting C-Channel Framework
Corrosion-resistant galvanized C-channel purlins and mounting rails produced for utility-scale solar photovoltaic ground racking arrays under wind-load stress.
Agricultural Clear-Span Grain Storage Facilities
Galvanized C/Z purlin framing providing durable anti-corrosive structural support for bulk agricultural grain sheds against humid rural environments.
Technical Overview
| Parameter | Information |
|---|---|
| Machine / Product Family | Automatic quick-change C/Z/U structural purlin roll forming line |
| Applicable Coil Materials | Hot-dip galvanized steel, cold-rolled steel (Q235, Q355, S350GD, S550GD) |
| Material Thickness Range | 1.50 mm – 3.00 mm (optional heavy-duty up to 3.50 mm) |
| Web Height Range (H) | 80 mm – 300 mm (motorized stepless adjustment via PLC) |
| Flange Width Range (B) | 40 mm – 80 mm (independent motorized width adjustment) |
| Lip Length Range (C) | 12 mm – 25 mm (inward structural stiffening return lips) |
| Forming Stations & Tooling | 14 – 18 heavy-duty stands (solid GCr15 / Cr12MoV, HRC 58–62) |
| Punching System | Multi-station hydraulic pre-punching for web & flange slotted bolt holes |
| Cutting System & Shear Blade | Universal stepless hydraulic or servo flying shear (Cr12MoV, no blade change) |
| Line Speed & Length Accuracy | 15 – 35 m/min production speed; cut-to-length tolerance ±1.0 mm |
Related Solutions
C/Z Purlin Interchange Line Solution
C/Z interchangeable purlin line for plants that run both C and Z. Dedicated C or…
C & Z Purlin Combined Production Line
One line produces both C and Z purlins with quick tooling change. Ideal for meta…
C-Purlin Production Line for Roof Systems
Complete cold roll forming solution for C-section purlins used in metal building…
Z-Purlin Roll Forming Solution
Dedicated Z-purlin line for overlapping roof purlin applications. Lap joint desi…
Roof & Wall Purlin System Solution
Secondary steel for roofs and walls is a section family first: dedicated C, dedi…
Pre-Engineered Building Component Line
Integrated solution for PEB secondary framing: C/Z purlins, girts, eave struts,…
Related Information

What Is a CZ Purlin Roll Forming Machine? Specs, Changeover & RFQ Guide
Define CZ purlin roll forming machines: dual C/Z profile capability, changeover…
Read More
C/Z Purlin Quick Changeover Roll Forming: How Fast Can It Switch?
C-to-Z purlin changeover in 15 minutes or 4 hours? A practical guide to quick-ch…
Read More
How Does a CZ Purlin Roll Forming Machine Work?
Learn how CZ purlin roll forming machines work: from decoiling to precision cutt…
Read More
C Purlin vs Z Purlin: Structural Differences, Spanning, and Sourcing Guide
Compare C vs Z purlins for structural strength, spanning, and installation. Lear…
Read More
How to Choose a CZ Purlin Roll Forming Machine: Technical & Sourcing Guide
Guide to choosing a CZ purlin roll forming machine: evaluate tolerance, servo-cu…
Read More
CZ Purlin Machine RFQ Checklist: What Buyers Must Specify
Essential RFQ checklist for CZ purlin machines: specify material strength, punch…
Read More
FAQ
How fast is profile changeover between C and Z profiles on an automatic purlin machine?
On automatic quick-change CZ purlin machines, size adjustments (web, flange, lip) take under 3 minutes via touchscreen servo control. Switching between C and Z profiles takes approximately 5 minutes by rotating roller cassettes 180 degrees or selecting profile mode in the PLC without disassembling roll shafts.
What coil thickness and yield strength range can standard purlin roll forming lines process?
Standard purlin roll forming lines process material thicknesses from 1.5 mm to 3.0 mm (standard) or up to 3.5 mm (heavy-duty) across structural steel grades spanning Q235, Q355, ASTM A653 Grade 50 (SS50), and EN 10346 S350GD to S550GD high-tensile galvanized strip.
What hydraulic punching hole patterns can be integrated into the purlin line?
Lines incorporate multi-cylinder hydraulic pre-punching dies to punch round holes (Φ14 mm, Φ16 mm, Φ18 mm) and elongated slots (14×22 mm, 18×26 mm) in web centers, flange edges, and lap zones. Hole positions and pitches are fully programmable in the PLC to match structural engineering drawings.
Does the universal shear cut-off system require blade replacement when changing purlin sizes?
No. Advanced CZ purlin roll formers utilize a universal stepless hydraulic shear design with adjustable upper and lower blades. The shear automatically adjusts its cutting window alongside motorized profile resizing, cutting all C and Z profiles from 80 mm to 300 mm without changing cutter dies.
Stop-to-cut hydraulic shear vs. flying shear: which cut-off system is best for purlin production?
Stop-to-cut hydraulic shearing halts material briefly, providing simple operation, low maintenance, and speeds of 12–18 m/min. Synchronized servo flying shears track the moving profile without decelerating the mill, achieving continuous line speeds of 25–35 m/min with higher daily throughput and zero stop marks.
How are camber, bow, and twist controlled during high-strength purlin roll forming?
Lines integrate heavy-duty entry leveling rolls, multi-station progressive breakdown roll stands, and an omnidirectional 10-roller straightening head (Turk's head) at the line exit, allowing operators to fine-tune horizontal and vertical straightness to satisfy EN 10162 and ASTM A653 tolerances.
What critical specifications should buyers confirm before purchasing a purlin roll forming line?
Buyers should specify target profile range (C80–300, Z100–300, U-channels), maximum steel thickness and yield strength, roller material (Cr12 / GCr15 with vacuum hardening), forming shaft diameter (Φ80–90 mm), hydraulic punching cylinder count, and uncoiler capacity (5T to 10T).